Process Role: Gas Treating and Amine Manufacturing
The supplied references cover two distinct contexts. Gas sweetening uses circulating lean and rich solvent around absorption and regeneration. Amine manufacturing is chemical production and may include condensation, reboiling, evaporation and cooling, including recovery of unreacted ammonia. A published amine-production example is not evidence of a lean/rich gas-treating installation.
Gas Sweetening Thermal Integration
In the generic process logic, rich solvent from the absorber receives heat in the lean/rich exchanger before entering the stripper. Lean solvent from regeneration transfers heat to the rich stream, then passes through the lean cooler before returning to the absorber. The stripper also has a reboiler and an overhead condenser; each exchanger has a separate duty.
This is an application schematic, not a project piping drawing. The source diagram supplies no operating temperatures, flows or pressures.
Typical Thermal Duties
Lean/rich heat recovery and lean cooling
The lean/rich exchanger couples hot lean-solvent cooling with rich-solvent preheating. The lean cooler performs the remaining cooling duty required before solvent returns to absorption. Their stream conditions, heat loads and allowable pressure drops need separate selection.
Stripper reboiling and overhead condensation
The reboiler supplies heat to regeneration; the overhead condenser removes heat from vapour leaving the stripper. A suitable boiling or condensation configuration must be evaluated for that circuit rather than inherited from the lean/rich exchanger.
Amine-production evaporation and ammonia recovery
The amine-production references identify several thermal duties across a plant. One reference illustrates unreacted ammonia recovery through condensation followed by liquid subcooling. The condenser guide explains the published multi-pass arrangement; it is not a universal configuration.
Key Engineering Inputs
For gas treating, provide solvent type and concentration, lean and rich loading, contaminants, fluid properties, mass flows, inlet and target outlet temperatures, normal and limiting pressures and the pressure-drop margin. Supply fouling and corrosion history where available.
For ammonia recovery, identify vapour composition, condensation pressure, recovery or return requirements and cooling-water conditions. For reboiling or evaporation, give boiling conditions, vapour generation and circulation-system information. Do not combine these into one unqualified plant duty.
Design Challenges
Review thermal recovery, hydraulic limits and material compatibility together. Define deposit behaviour and maintenance access. Confirm the operating envelope separately from design limits, including startup and turndown.
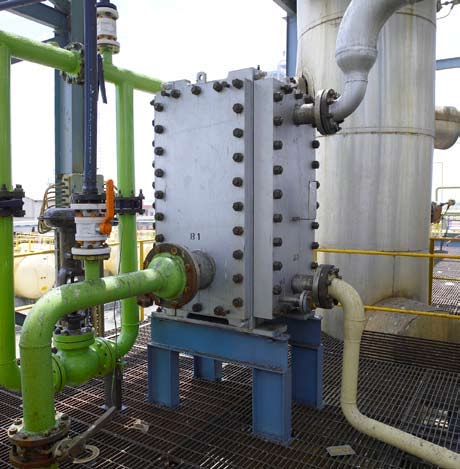
An anonymous gas-cleaning retrofit reference also highlights limited installation space. Use the actual equipment and piping layout to check footprint, connections and service clearances; do not infer valves or bypasses from a supplier schematic.
What PANSTAR Needs for Selection
Specify whether the enquiry concerns lean/rich solvent recovery, lean cooling, a stripper reboiler, overhead condensation or amine-production ammonia recovery. Submit a separate duty sheet for each proposed exchanger, together with fluid analysis, thermal and pressure-drop requirements, material evidence and installation constraints. Plant-level historical steam savings are not a single-unit selection criterion.
Engineering background: Gas-sweetening schematic, p. 39; installation context, p. 12; Published amine-manufacturing duty contexts; Published ammonia recovery configuration. The examples describe published third-party equipment, not PANSTAR installations.