Plate tooling & forming
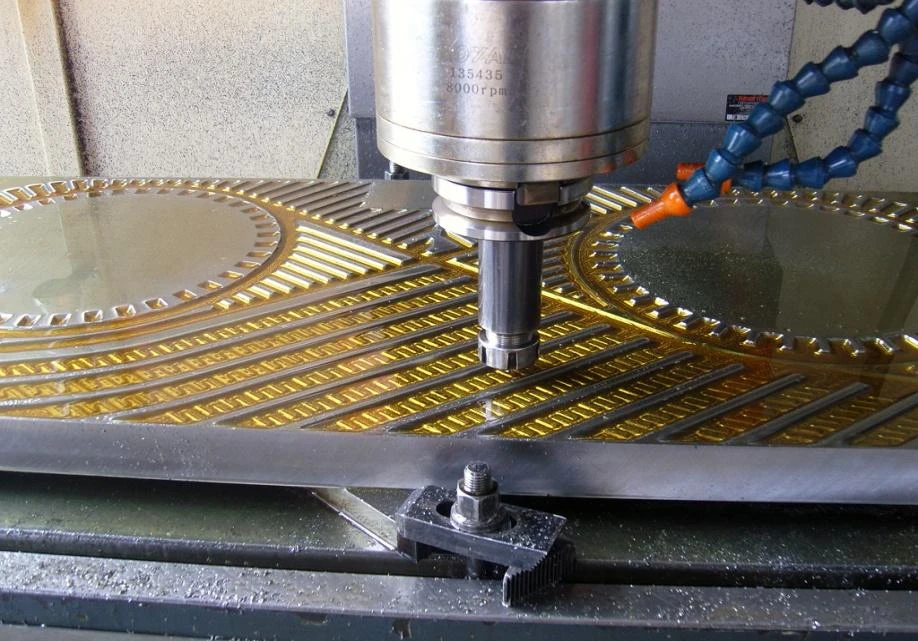
PANSTAR has in-house mould design and machining capabilities, supported by dedicated plate presses. Tooling defines the corrugation and edge geometry before the plates become a welded core.
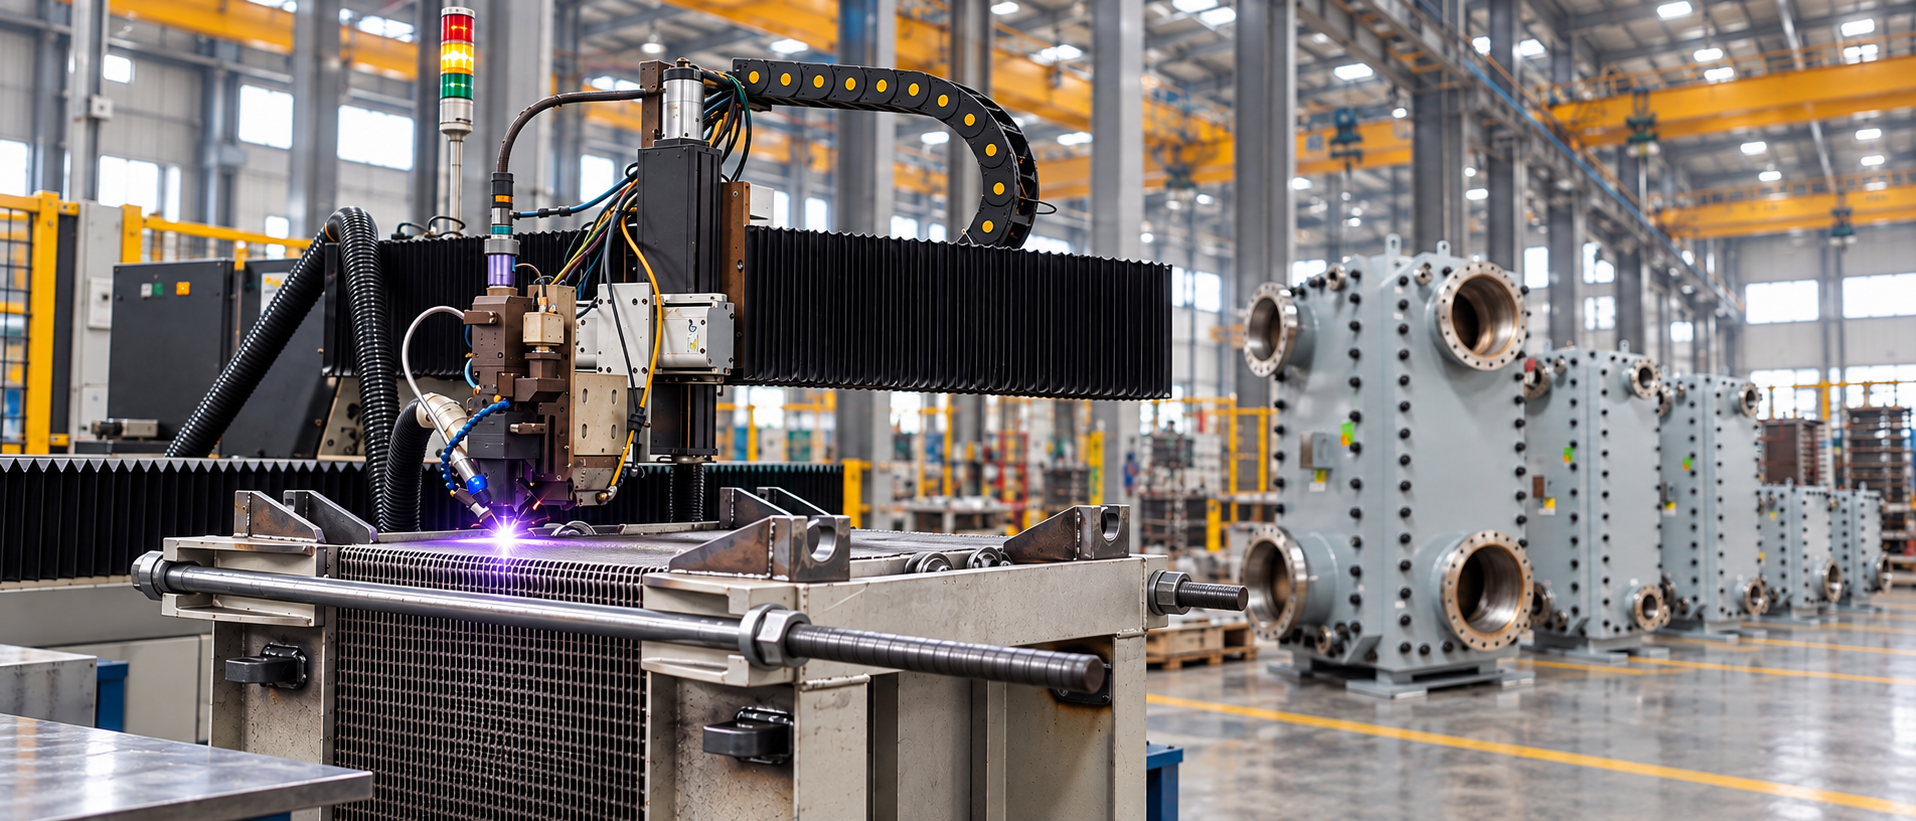
Plate forming, automated laser welding, assembly and inspection at PANSTAR’s manufacturing facility.
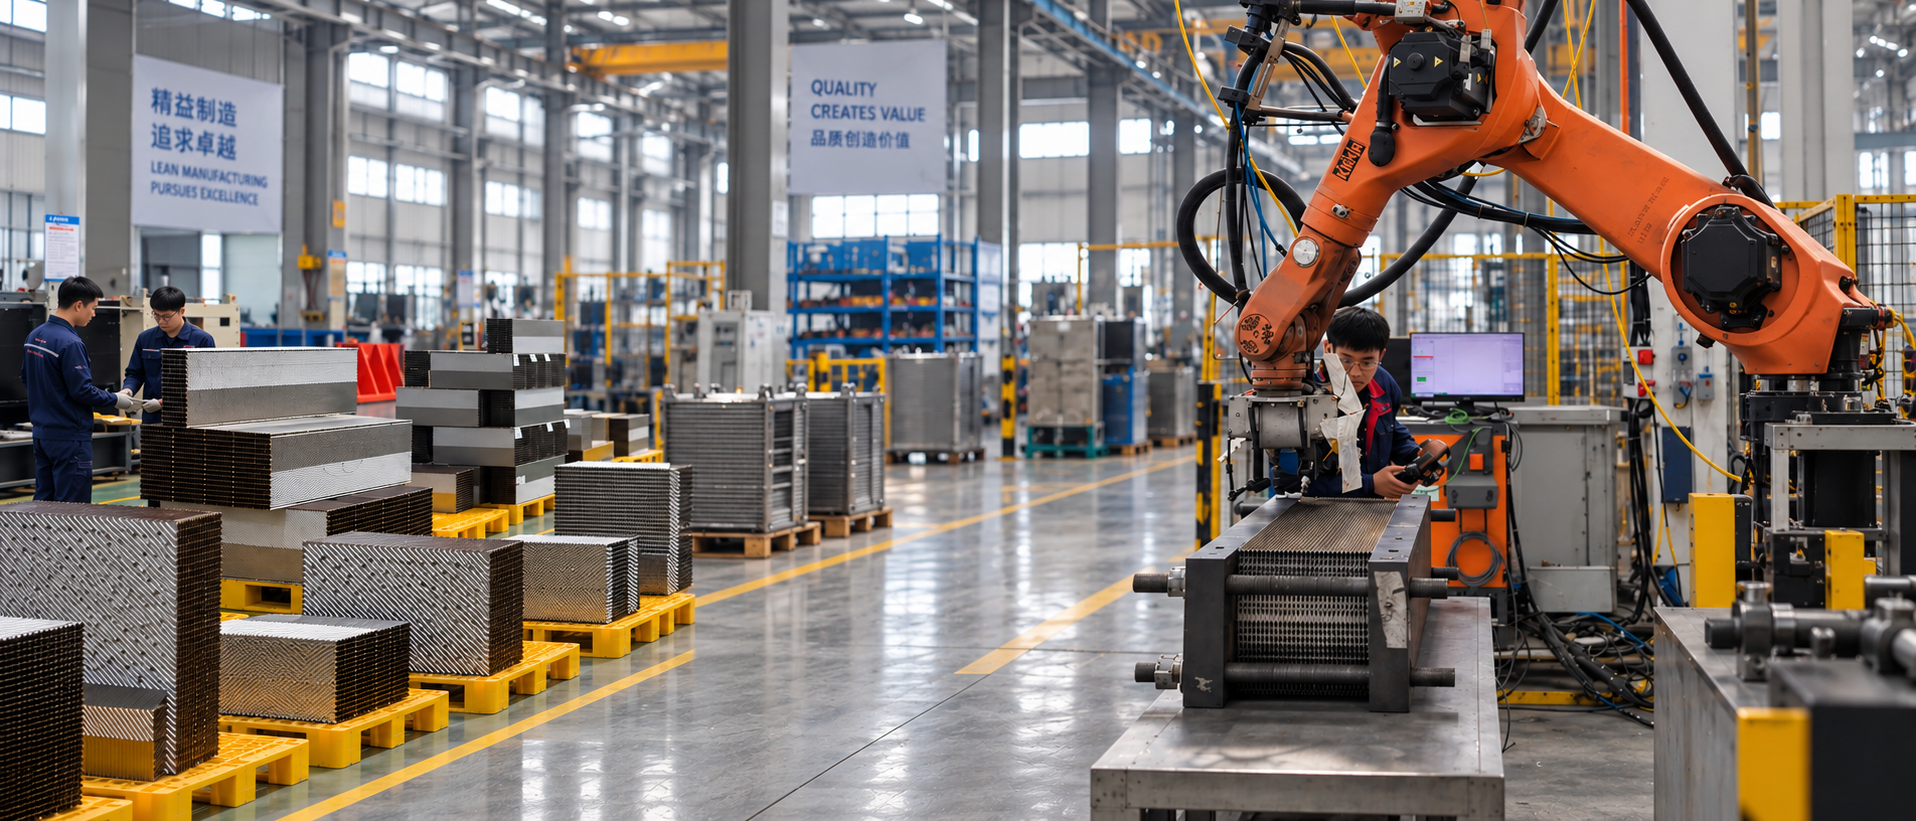
The Yangzhou site combines plate tooling, pressing and welding capabilities. PANSTAR also reports an in-house thermal test facility for product development.
No. 3, Jinyuan Road, Anyi Industrial Park,Closer views of the production stations used across PANSTAR’s heat exchanger manufacturing operations.
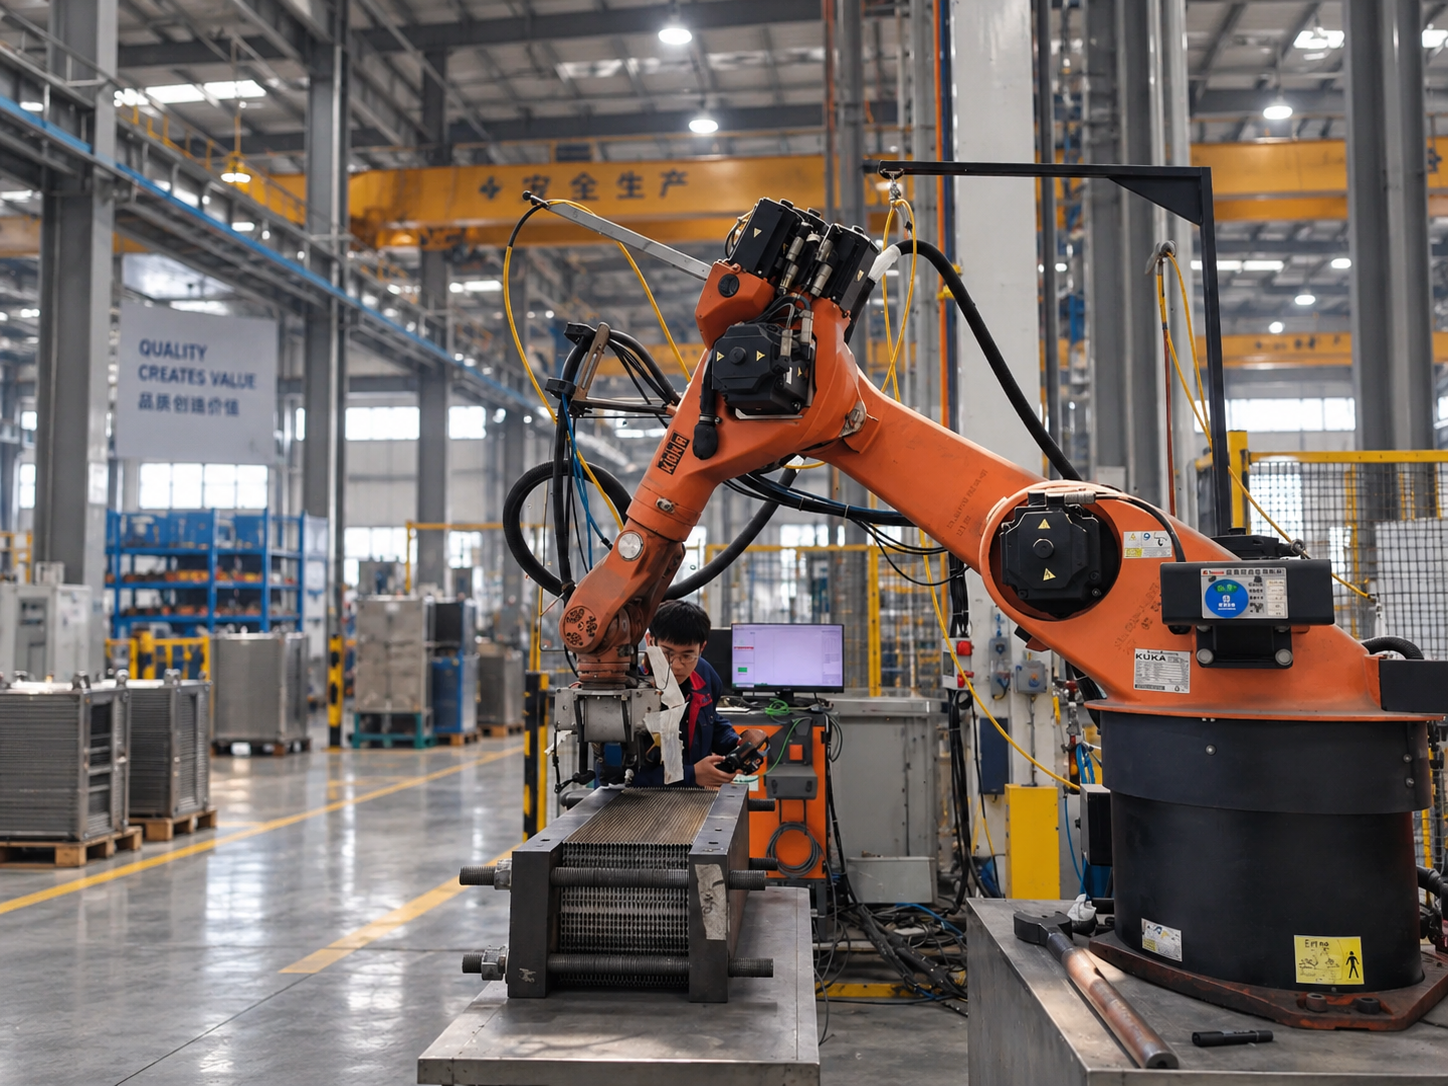
A robot and fixture position the work around a plate assembly.
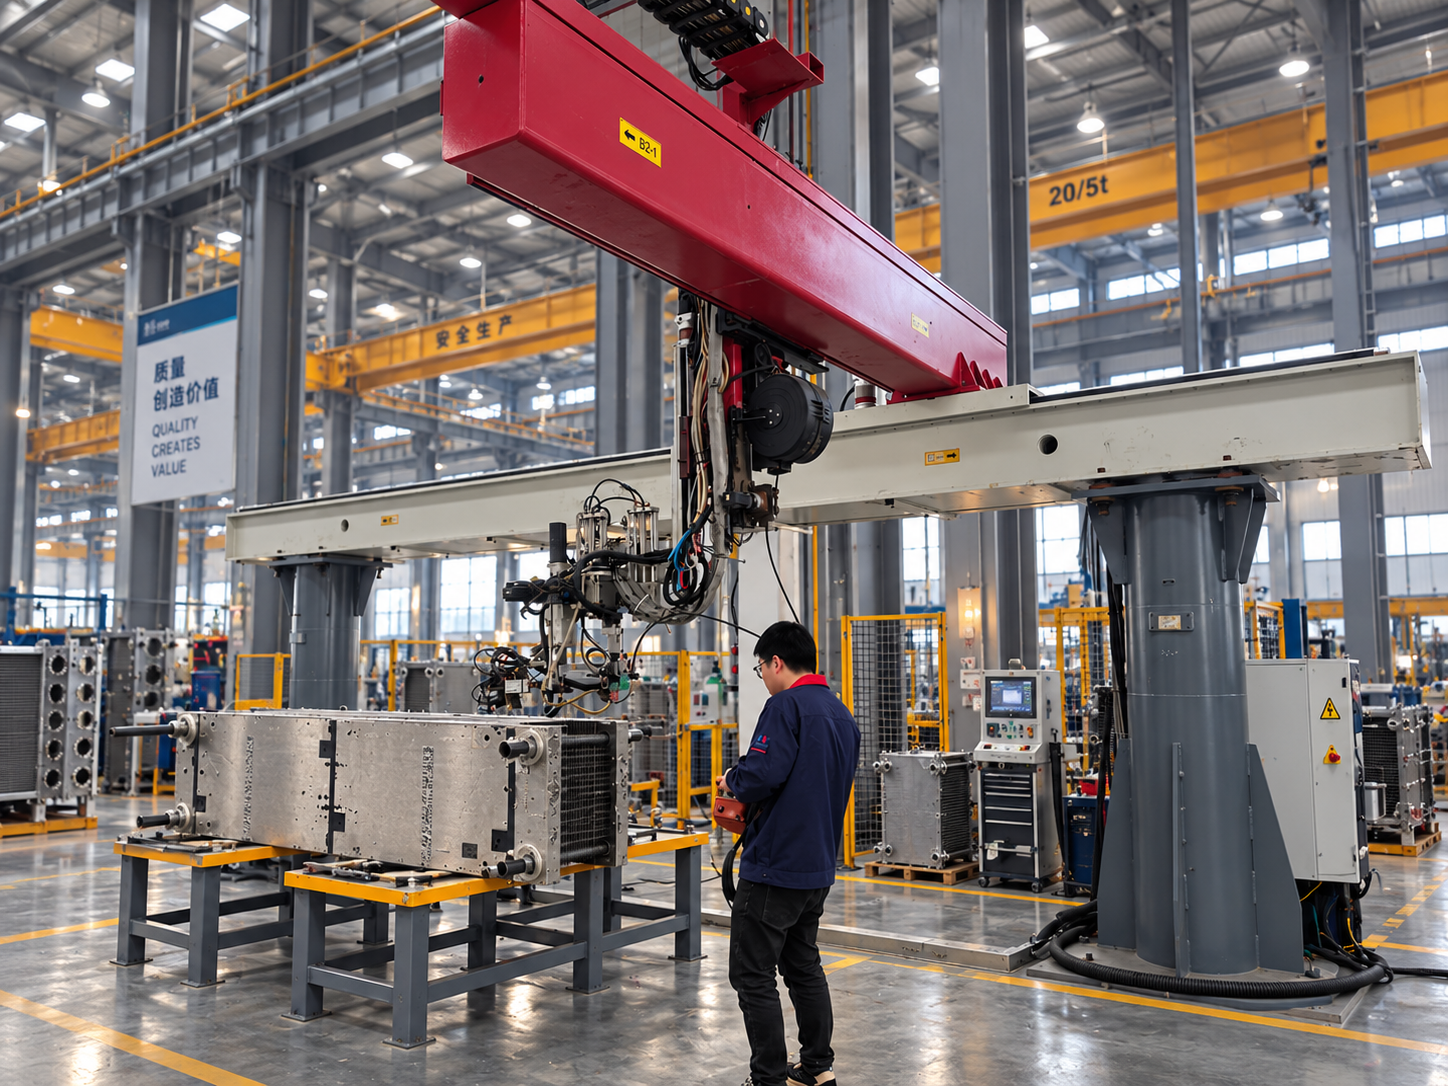
A clamped plate assembly beneath the gantry-mounted production equipment.
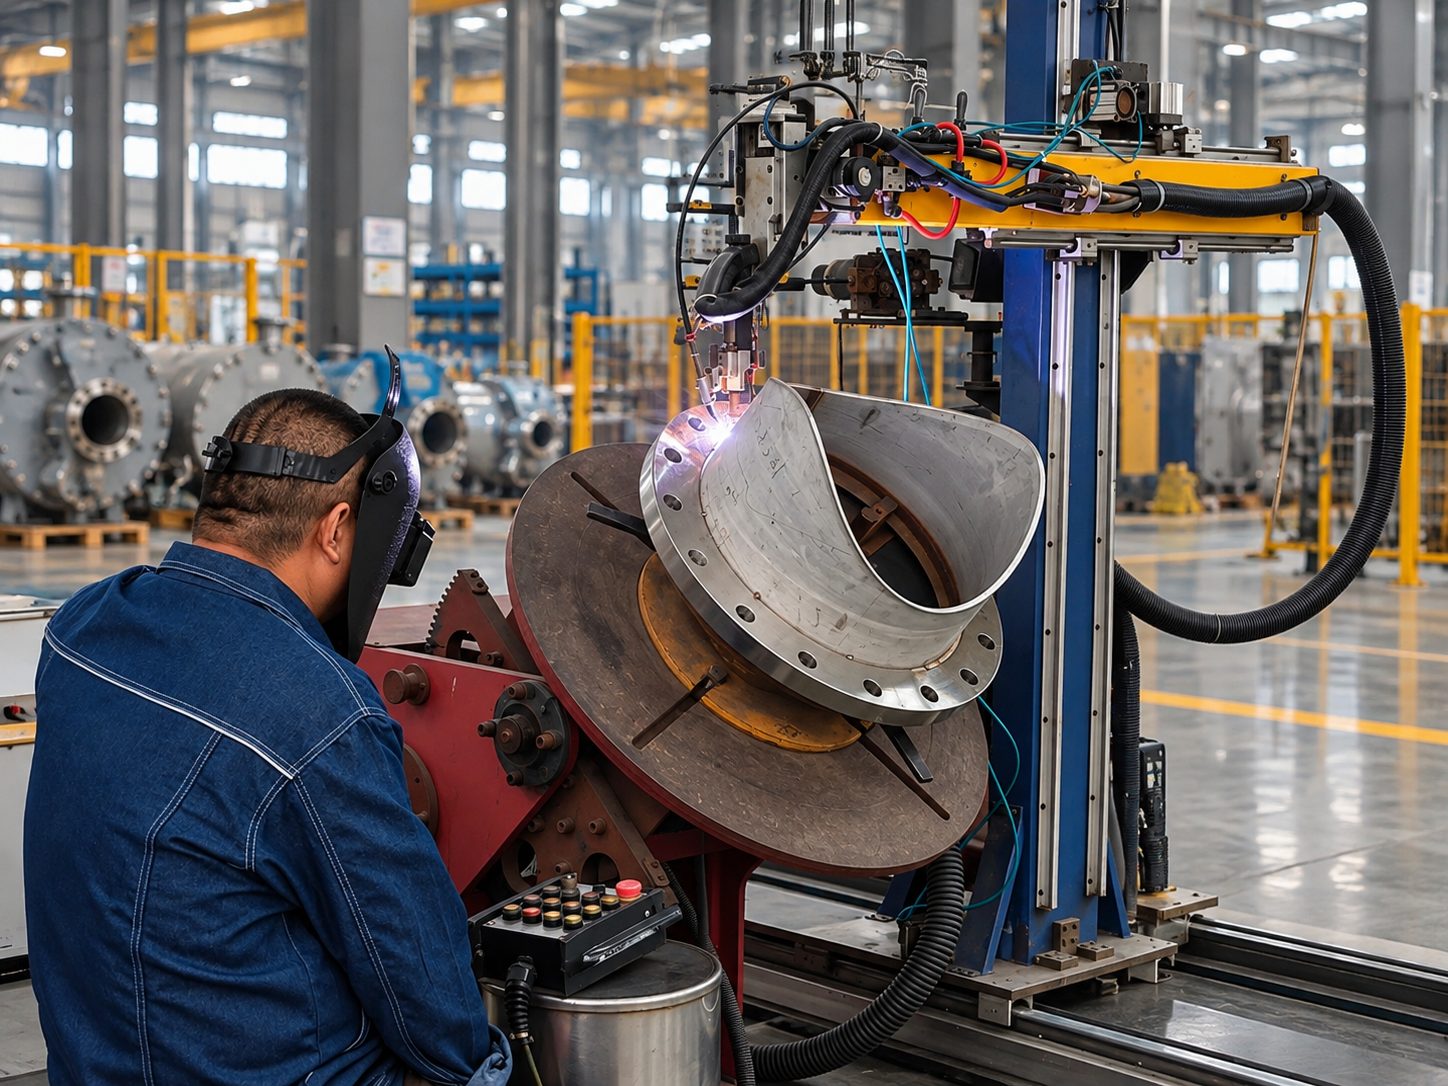
A flanged connection positioned for welding in the workshop.
PANSTAR has in-house mould design and machining capabilities, supported by dedicated plate presses. Tooling defines the corrugation and edge geometry before the plates become a welded core.
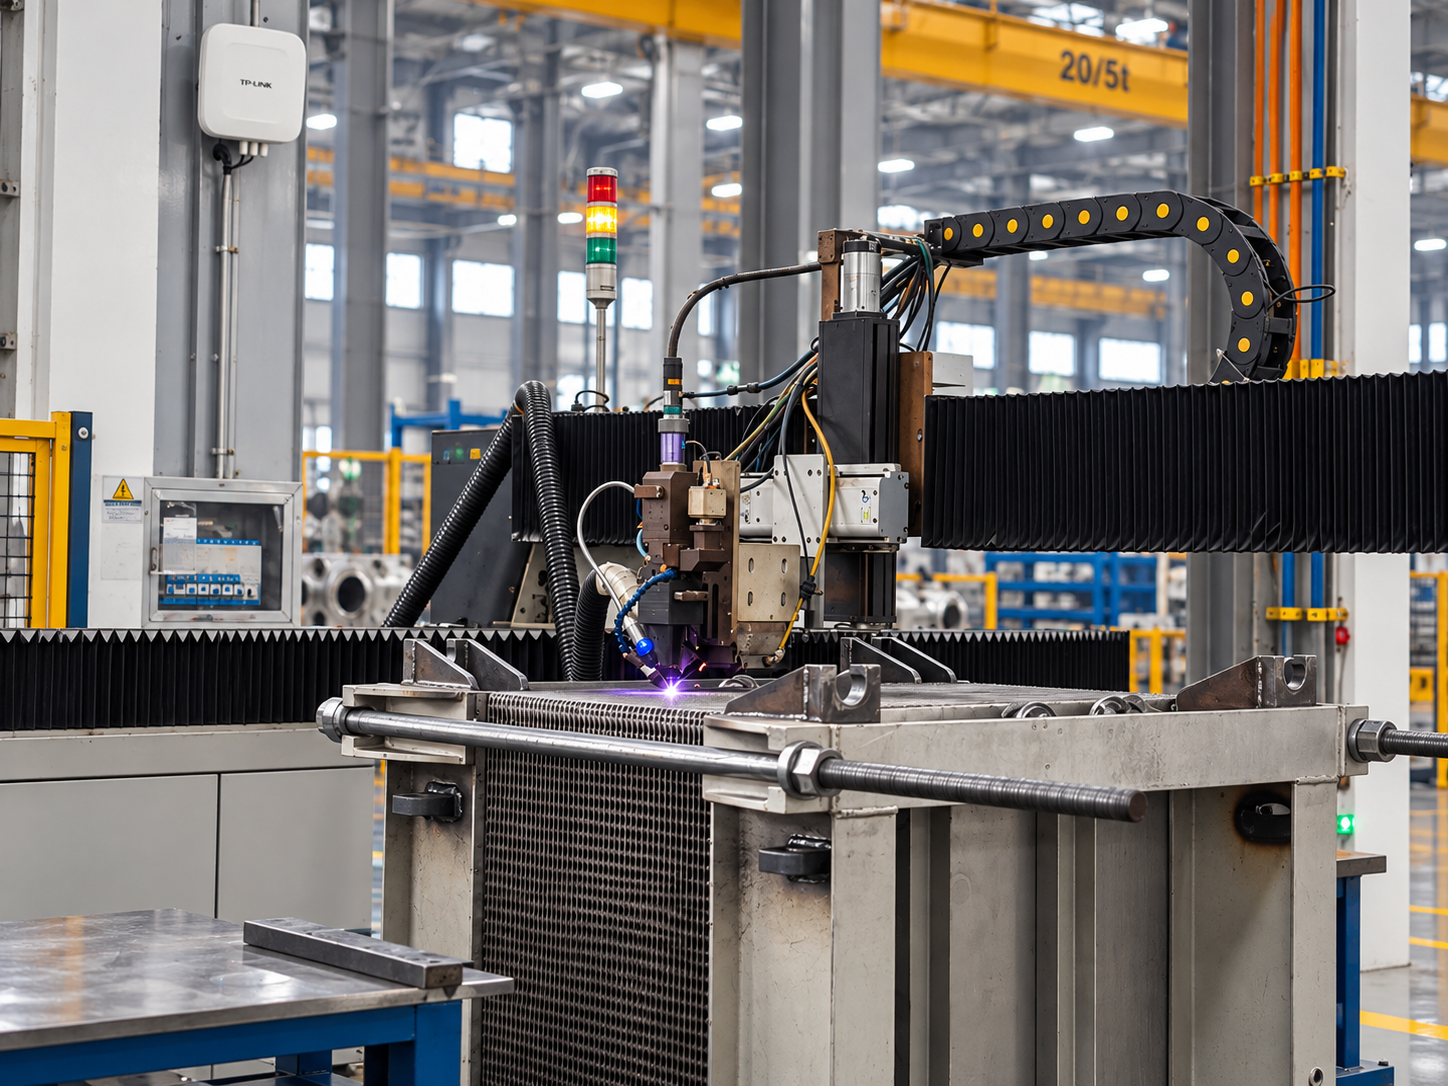
Laser-welding lines support welded heat exchanger production. Controlled positioning brings the plate edges together for repeatable welding along the channel boundaries.
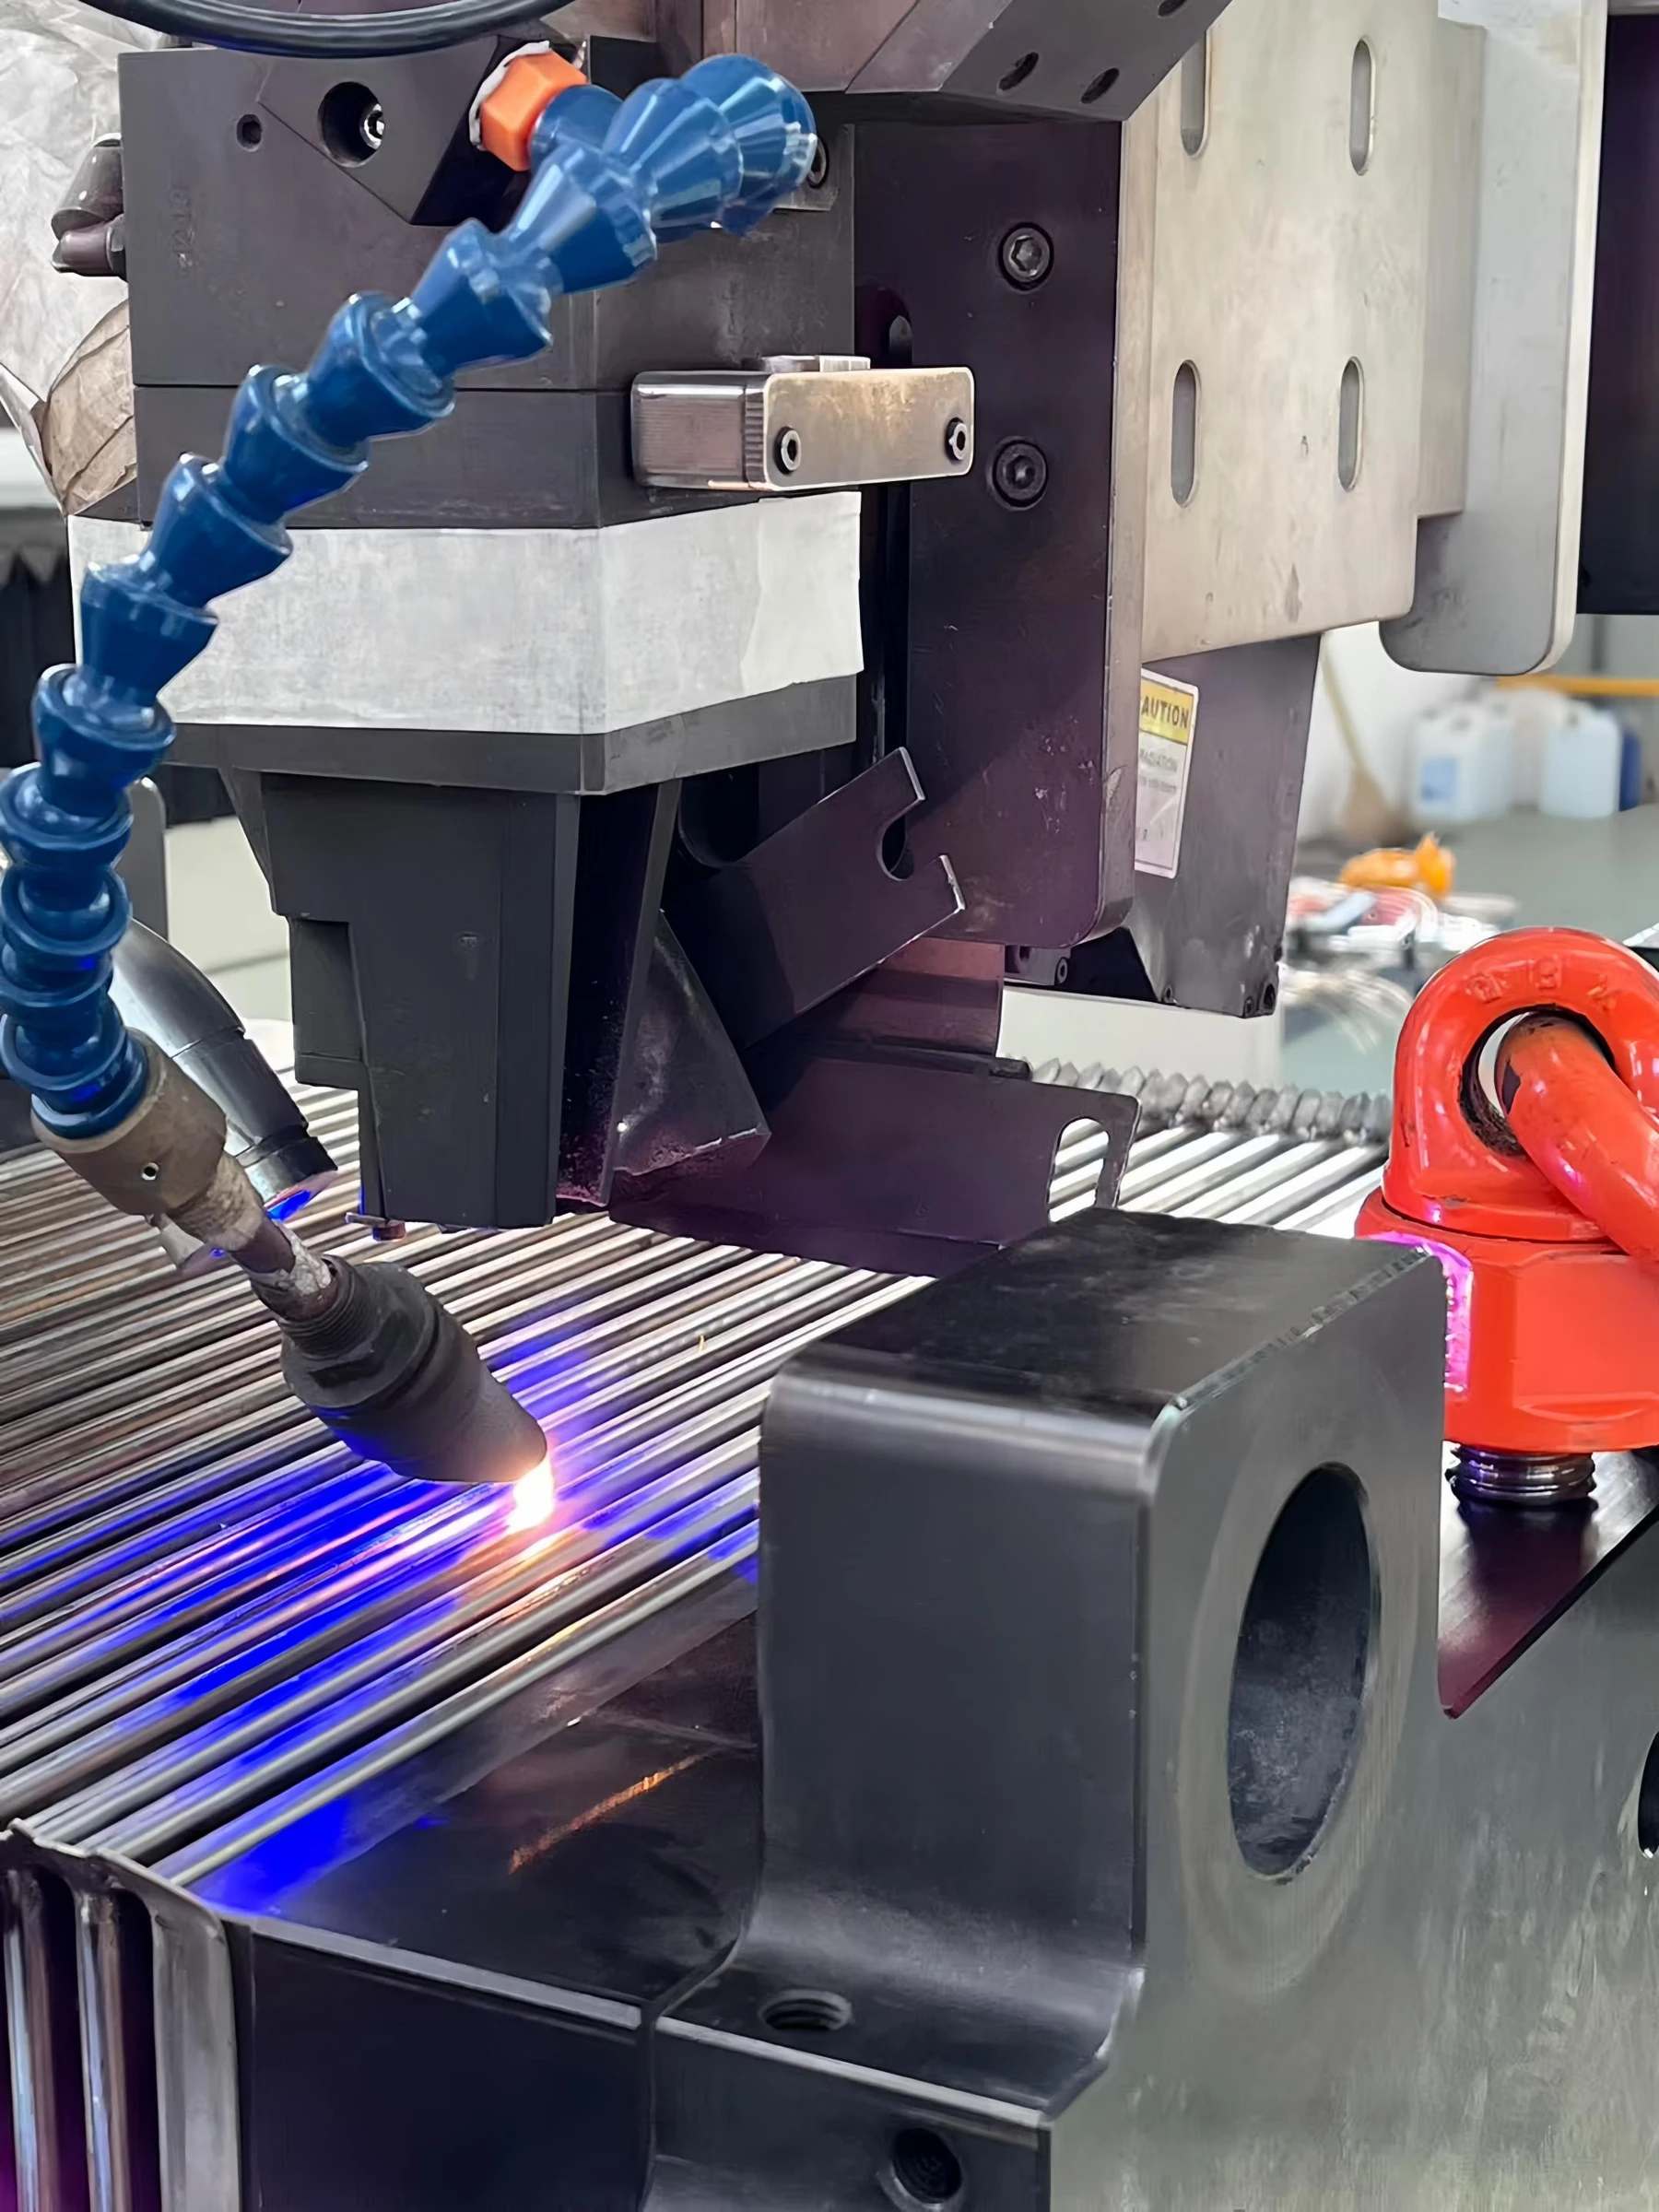
Adjacent plates are joined along alternating edge pairs to create two separate circuits. The narrow welded edges leave the formed passages open for flow.
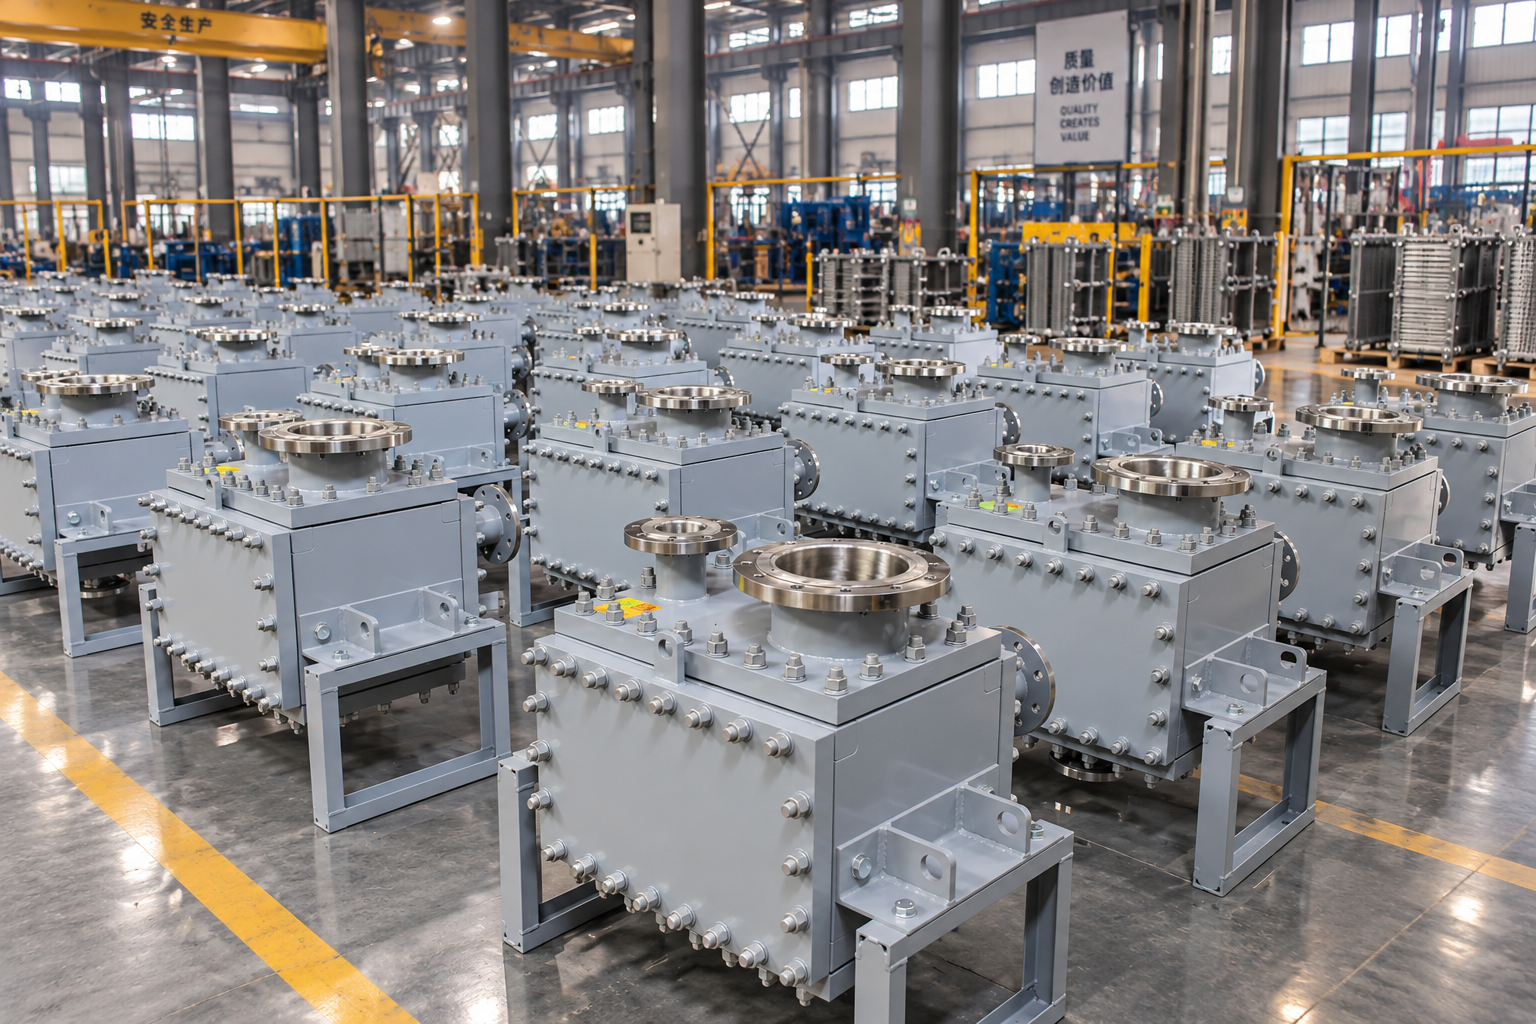
The welded core is enclosed by the frame and bolted side panels. Connections and internal flow arrangements are configured for the selected duty and installation.
Close-up production photographs show the formed plate surfaces and the channel openings of a welded core. Removable side panels provide access to the channel groups for inspection and cleaning.
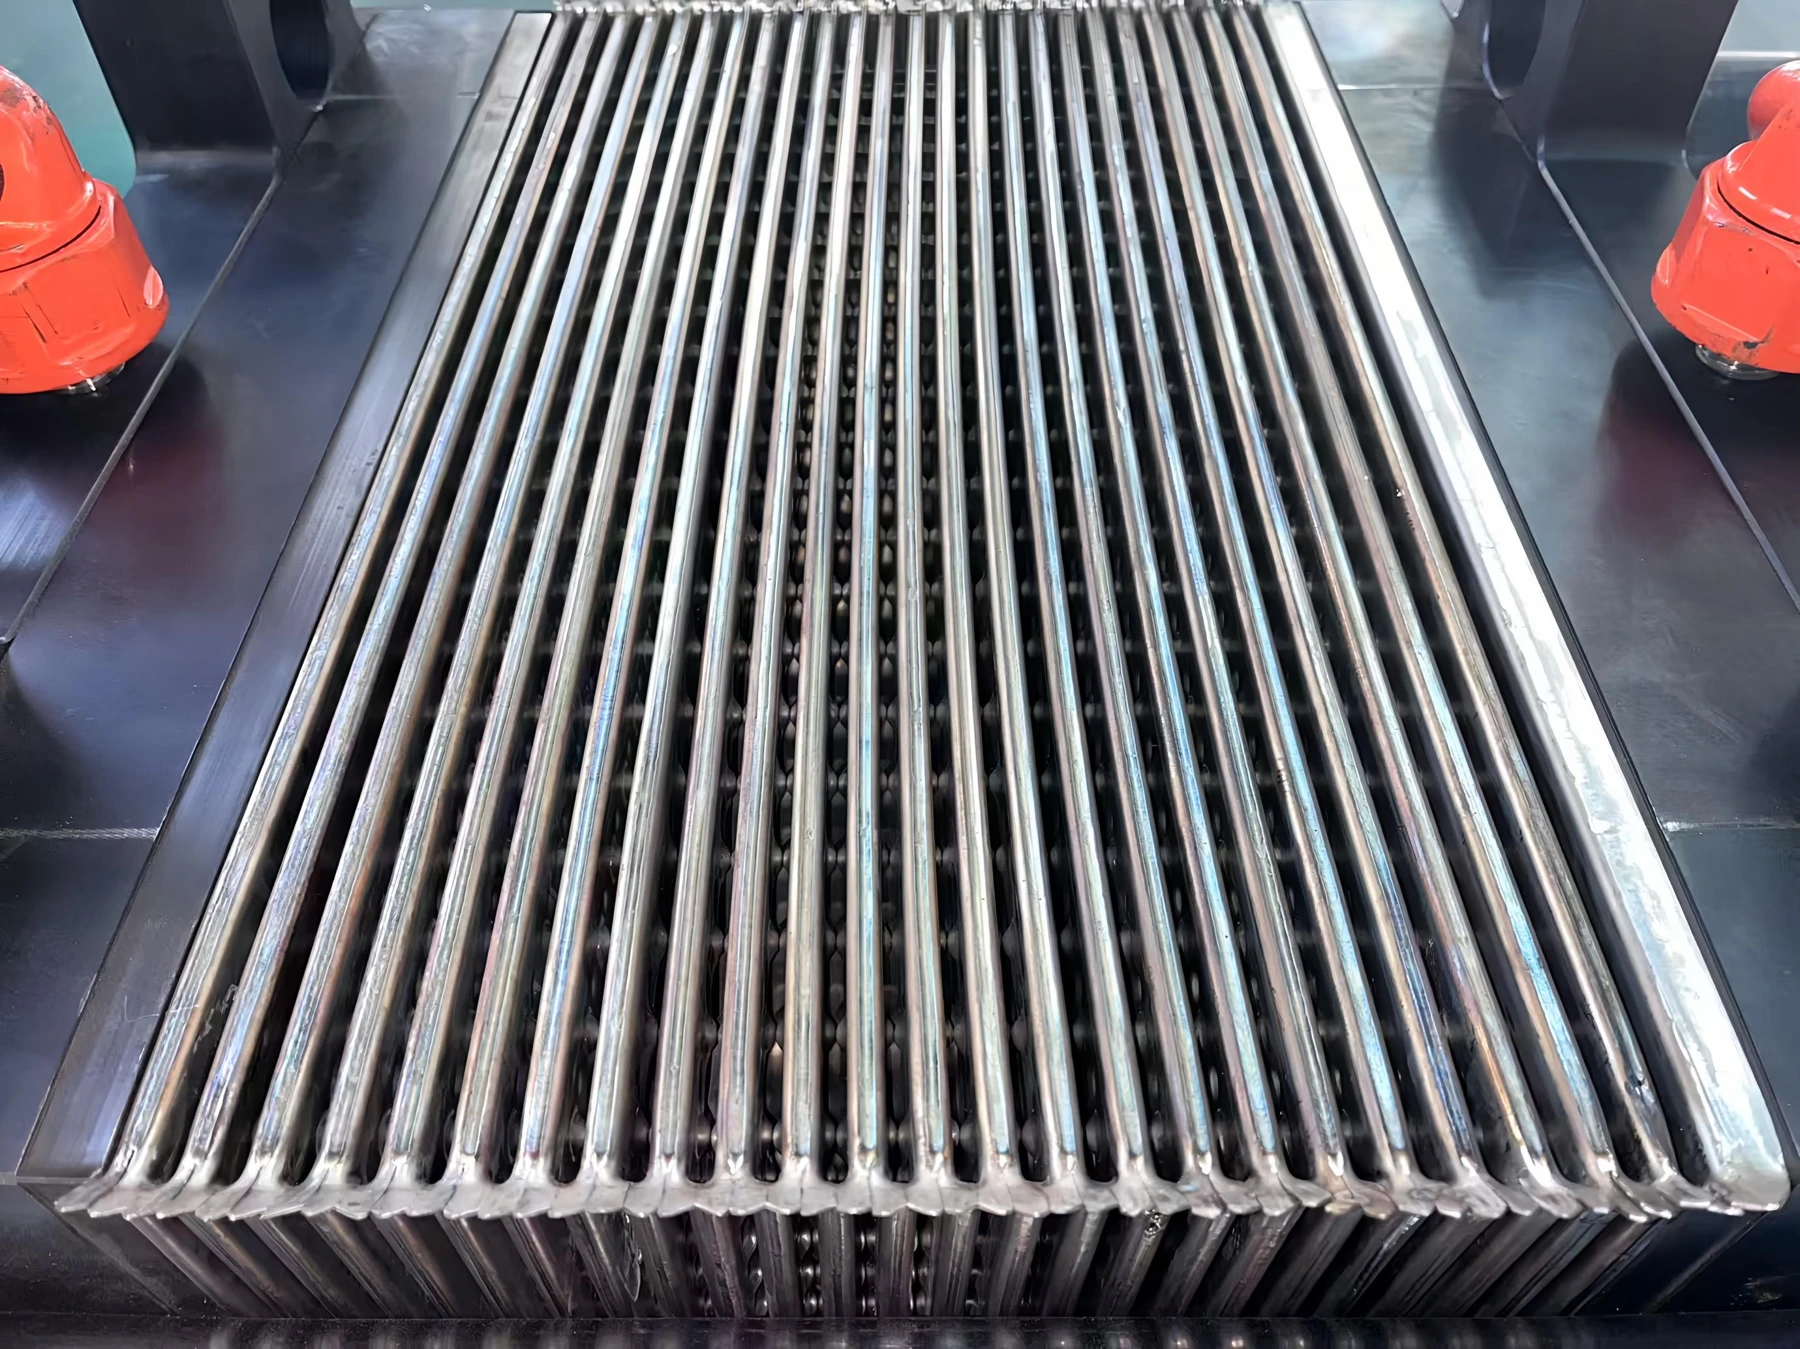
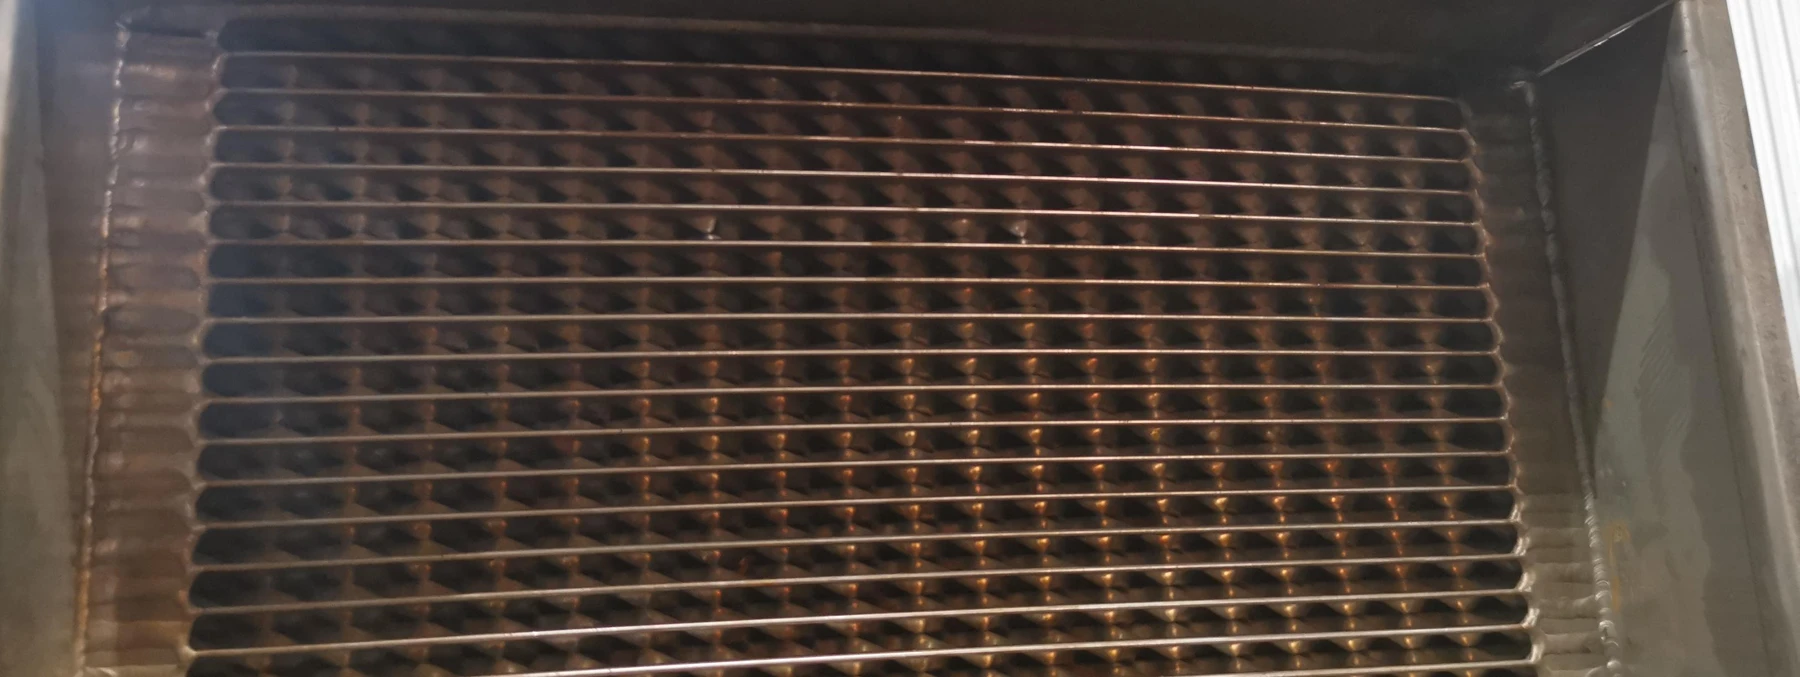
These production photographs follow real manufacturing, inspection and delivery stages—not just the finished equipment.
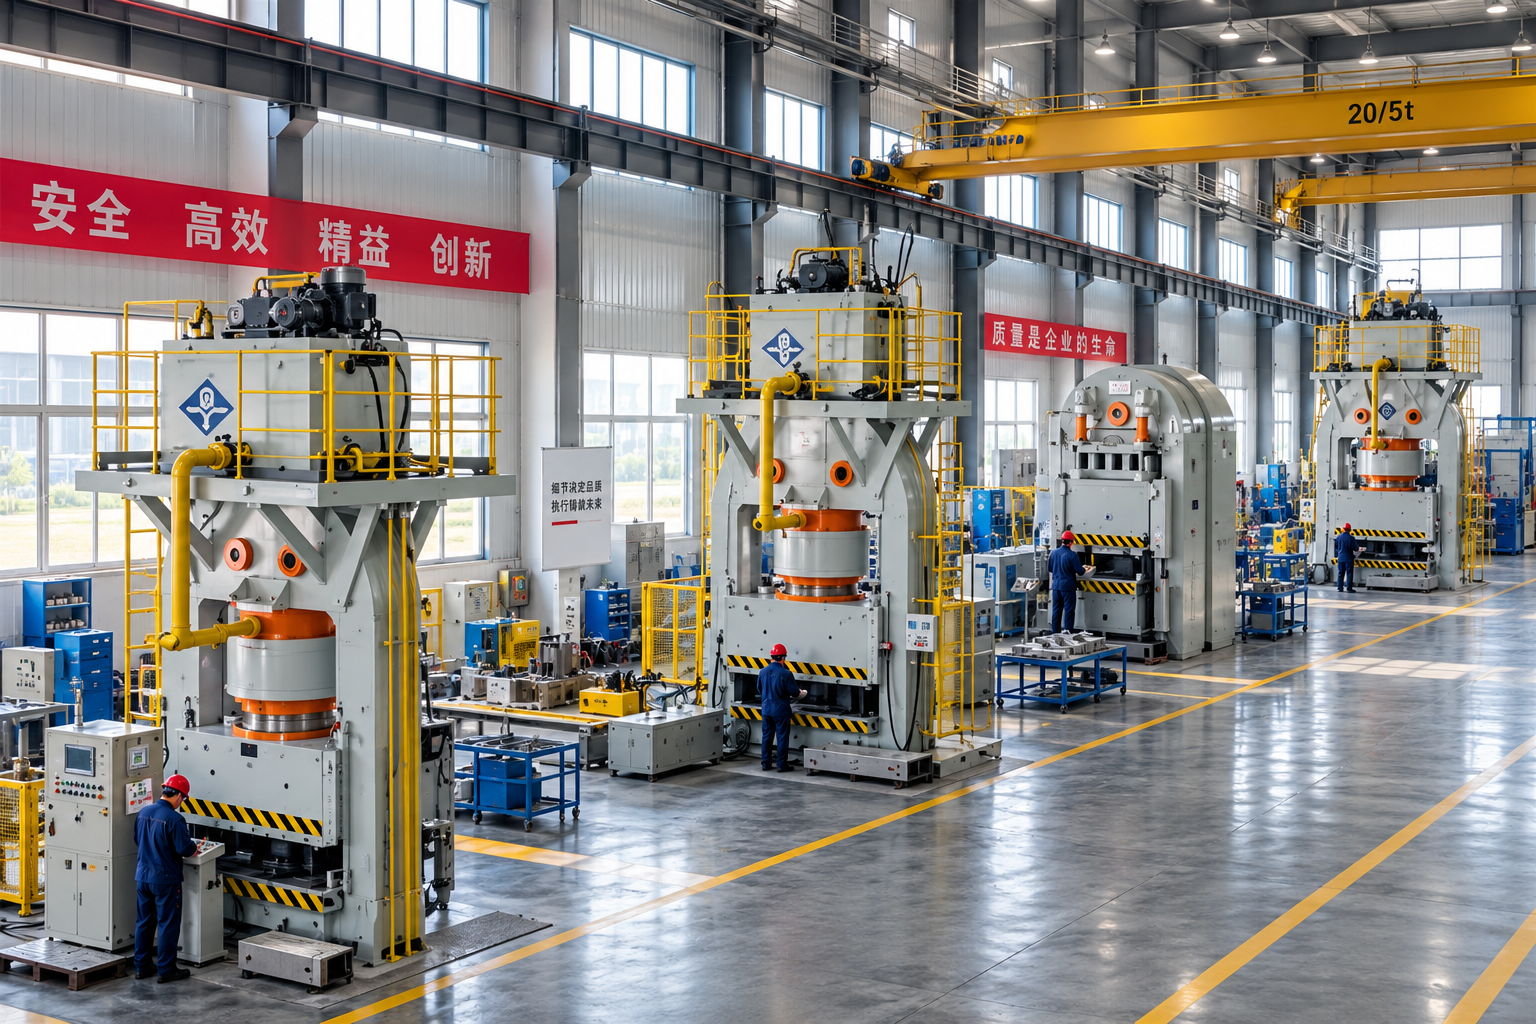
Dedicated presses and tooling form the plate geometry used in the welded heat-transfer core.
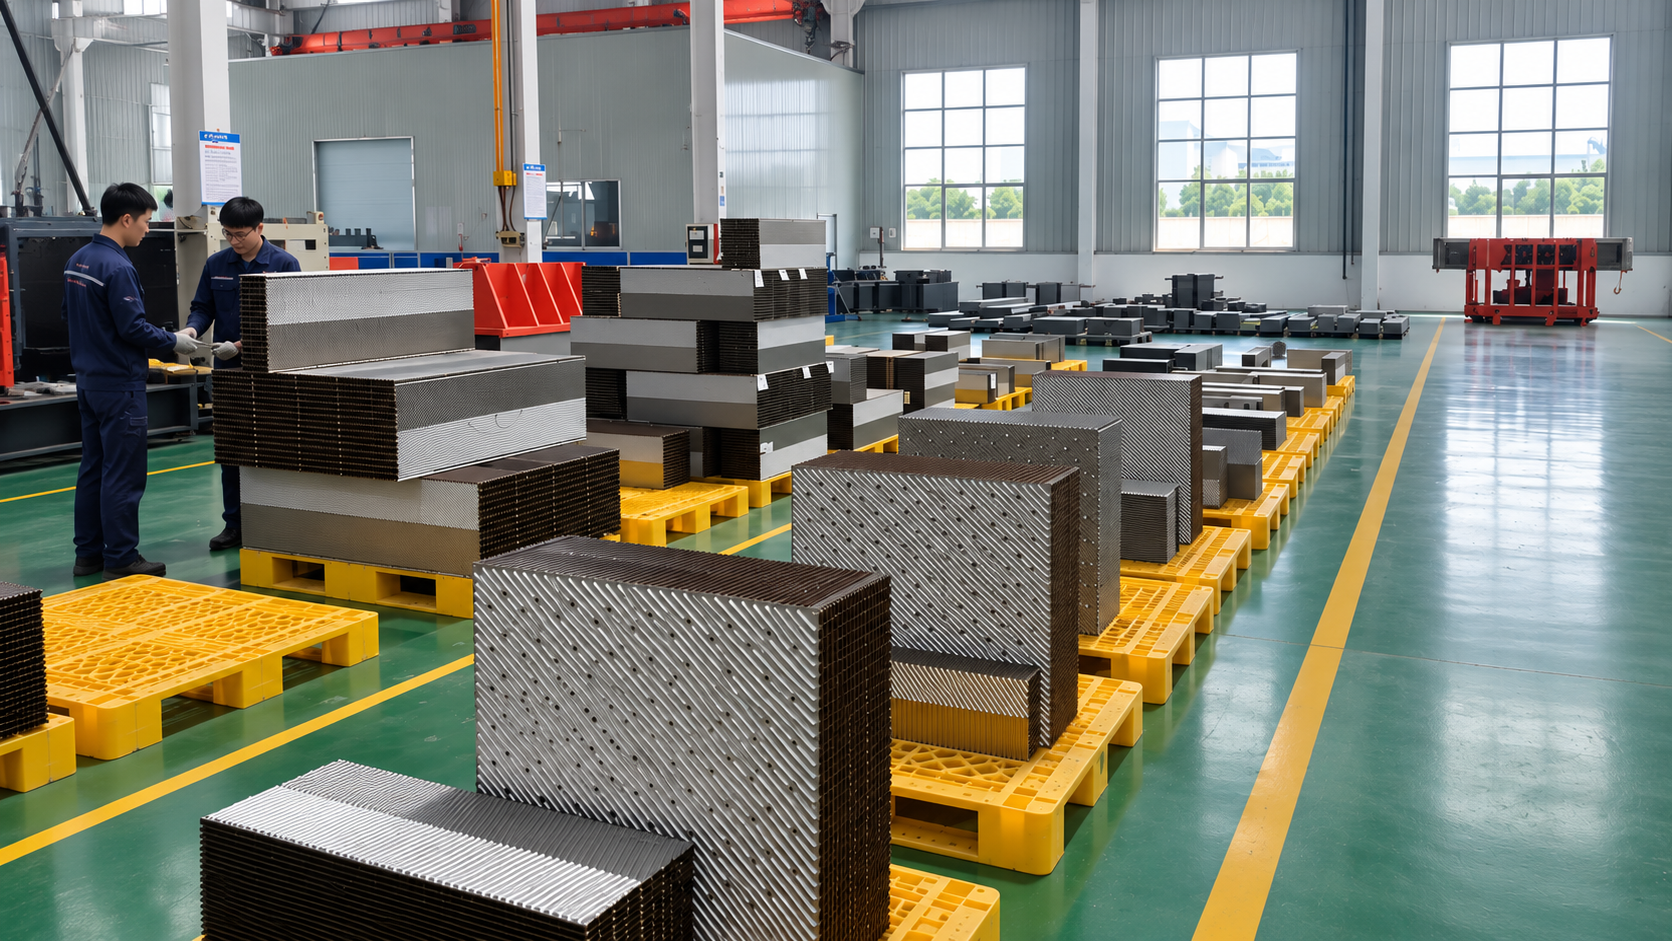
Plate sections are organized by size and project before the welded core is built.
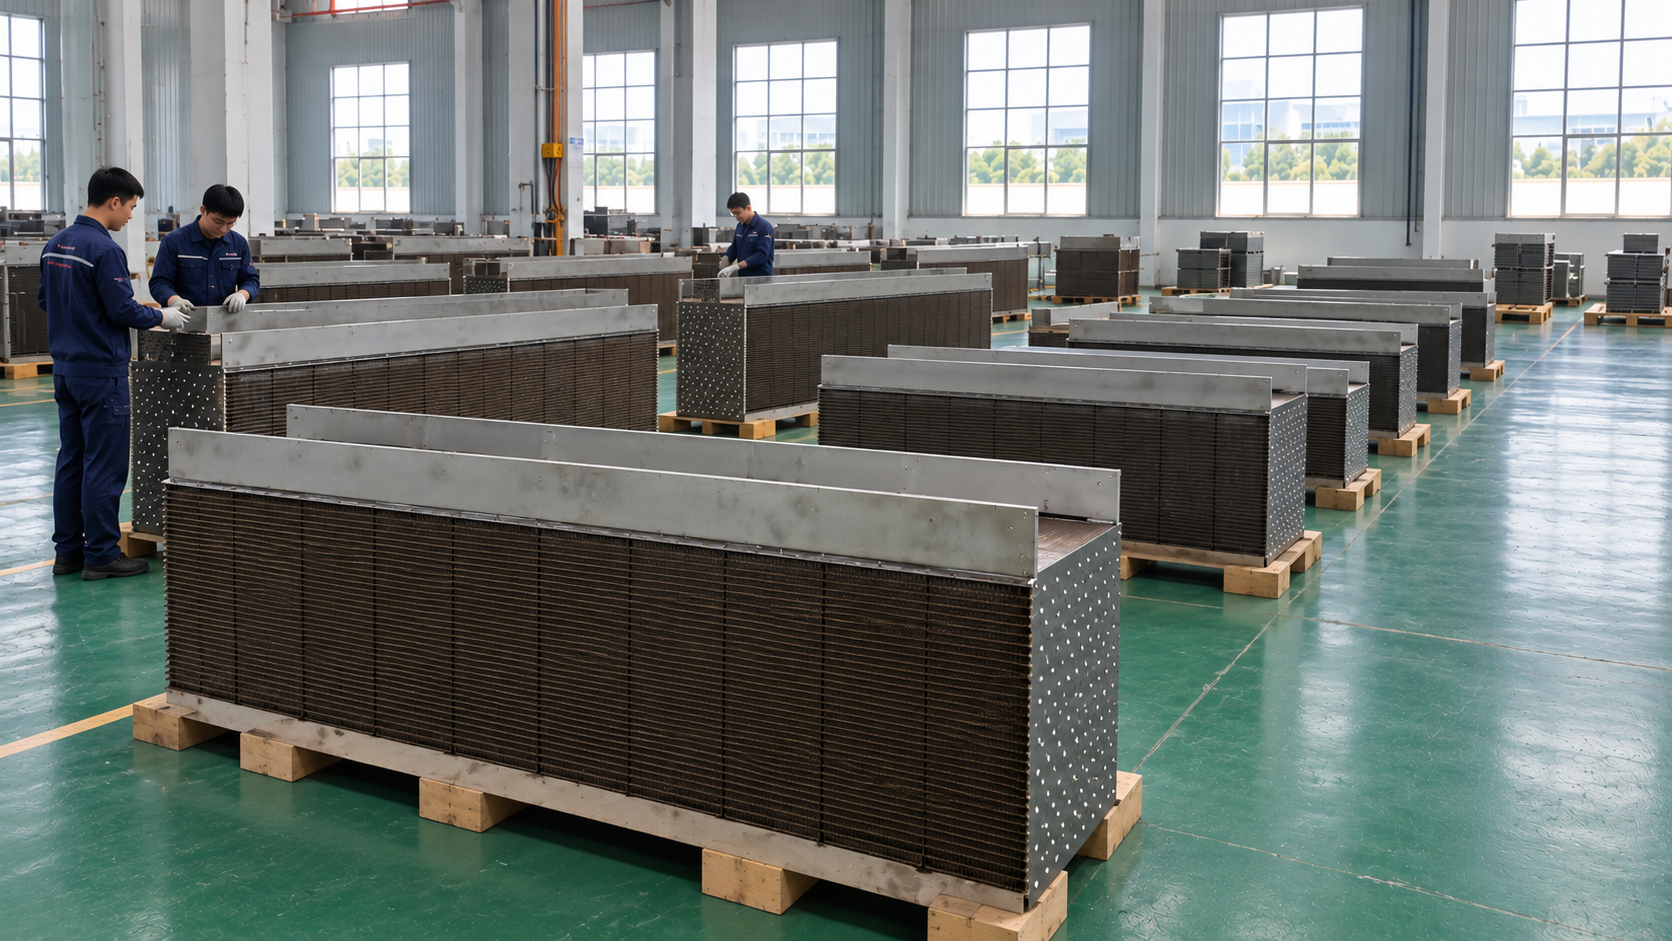
Completed plate packs at different sizes show the core geometry before final enclosure.
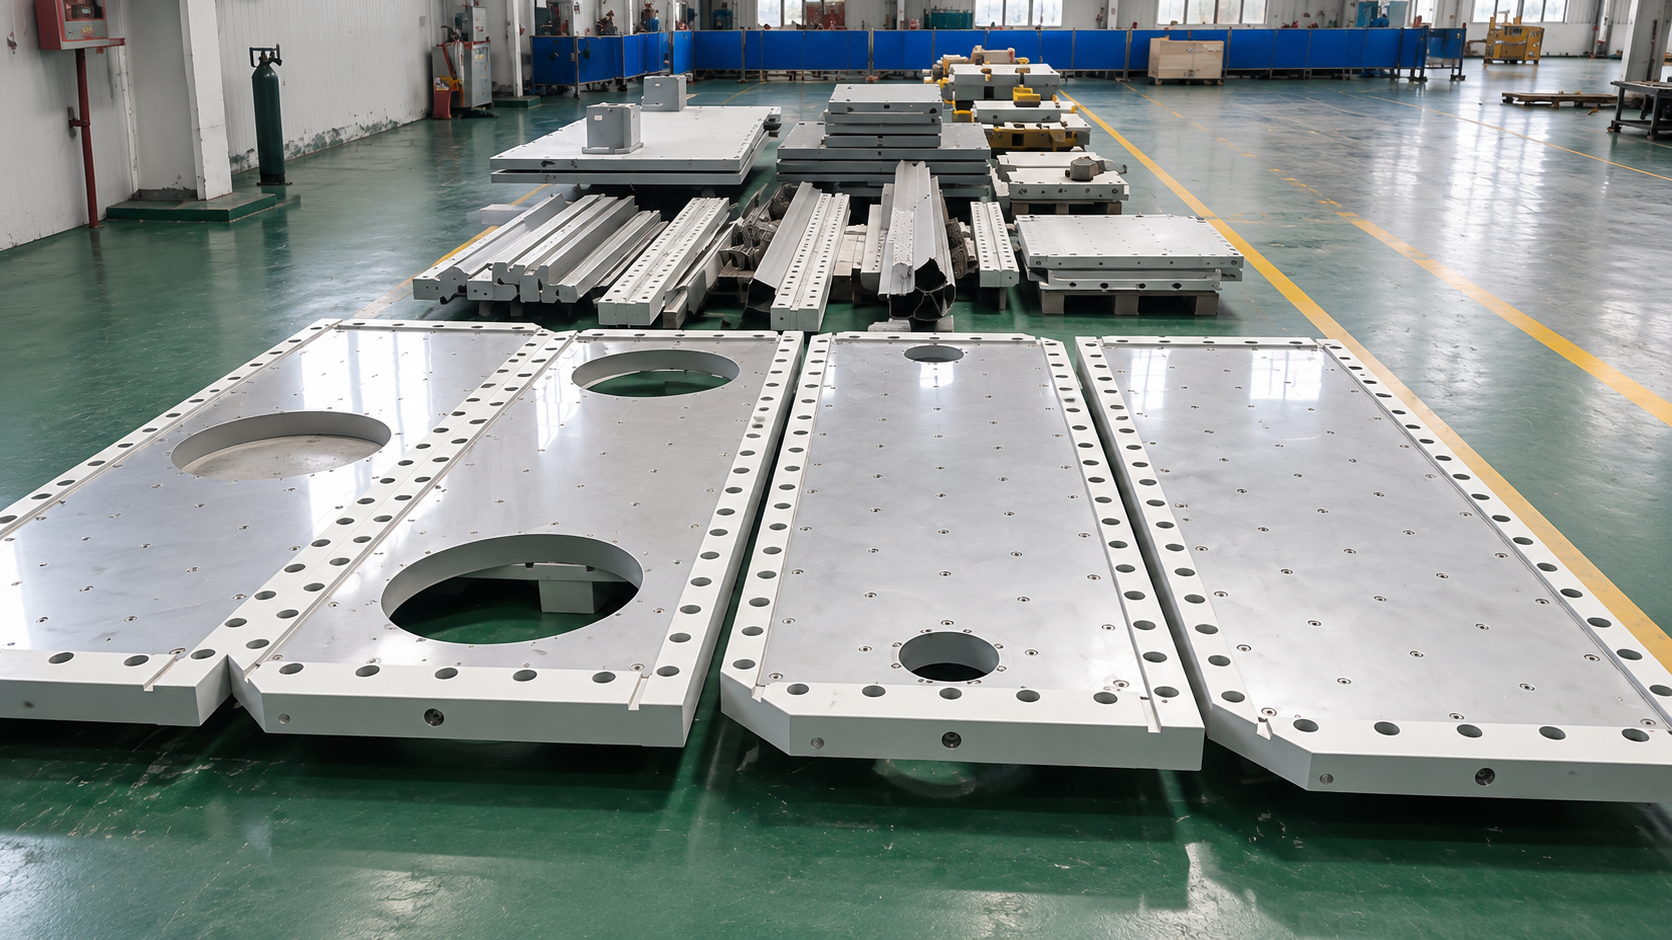
Panels, rails and support parts are prepared together for project assembly.
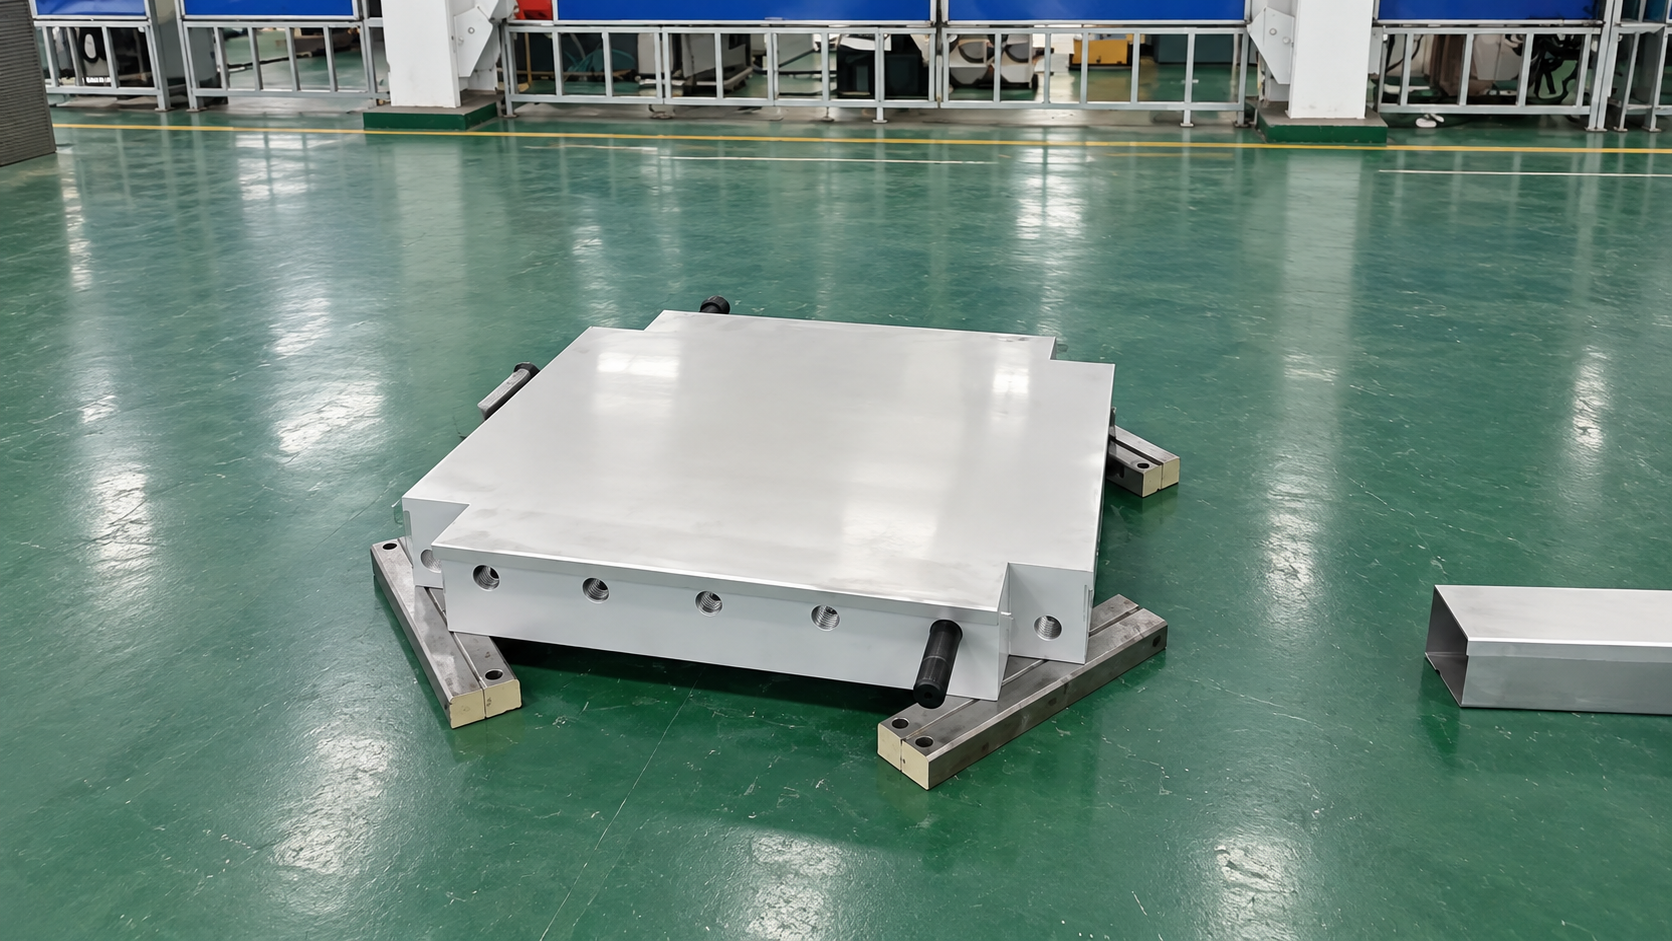
Machined support components are checked before they are fitted to the exchanger frame.
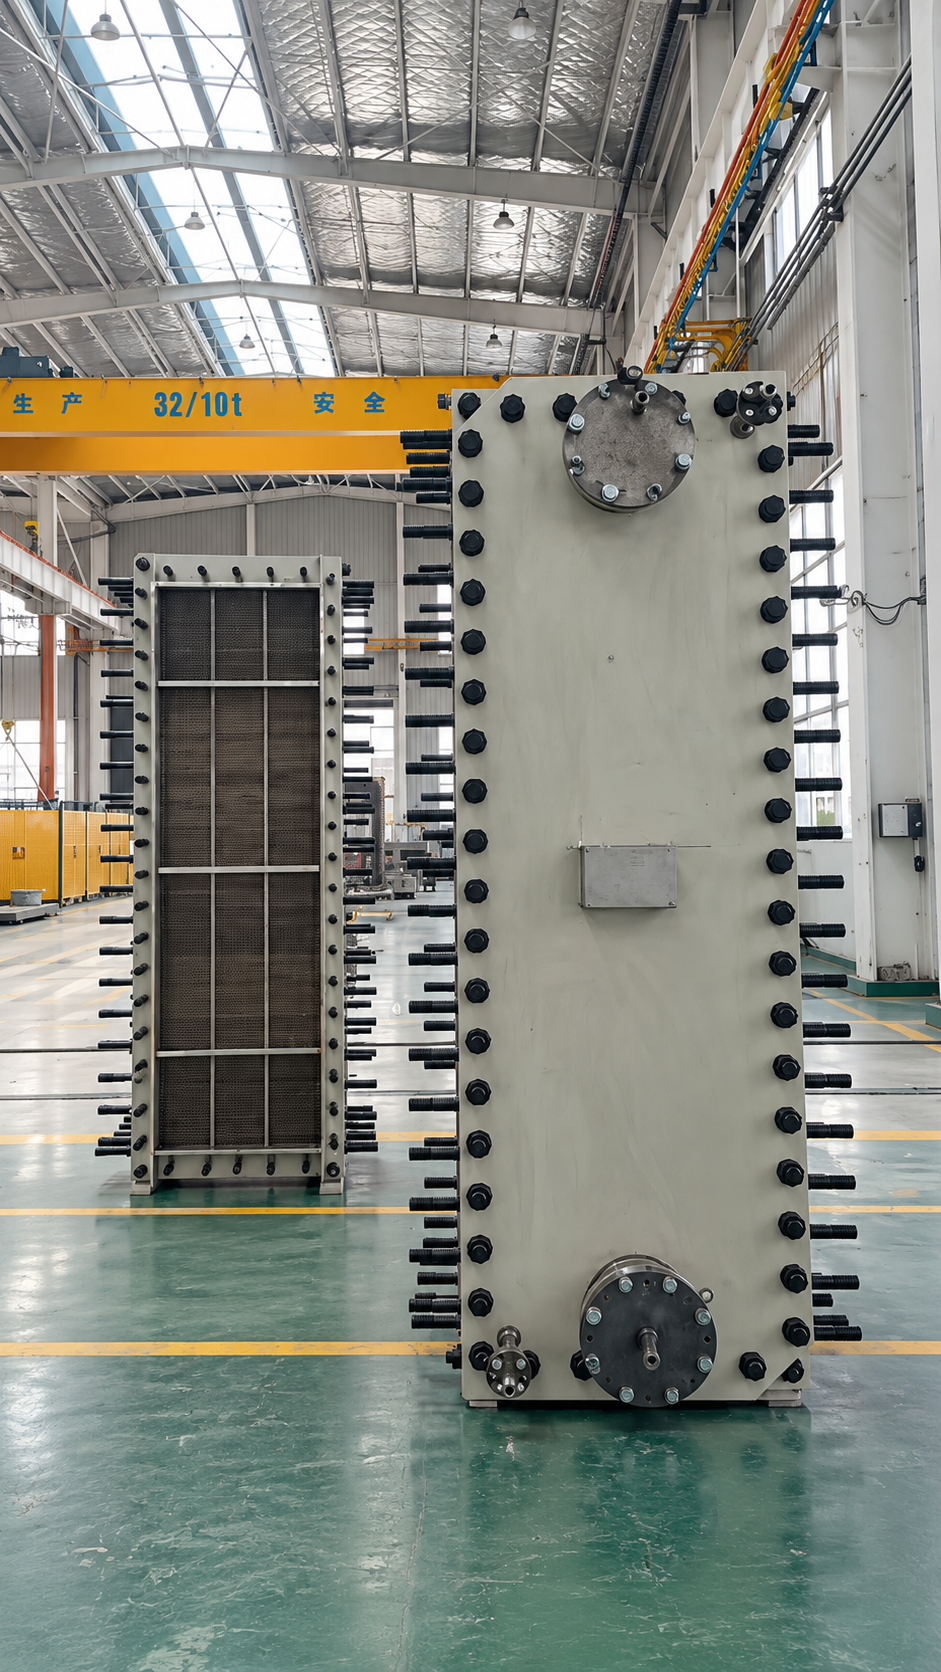
Side panels, studs and connections are fitted and checked before final assembly.
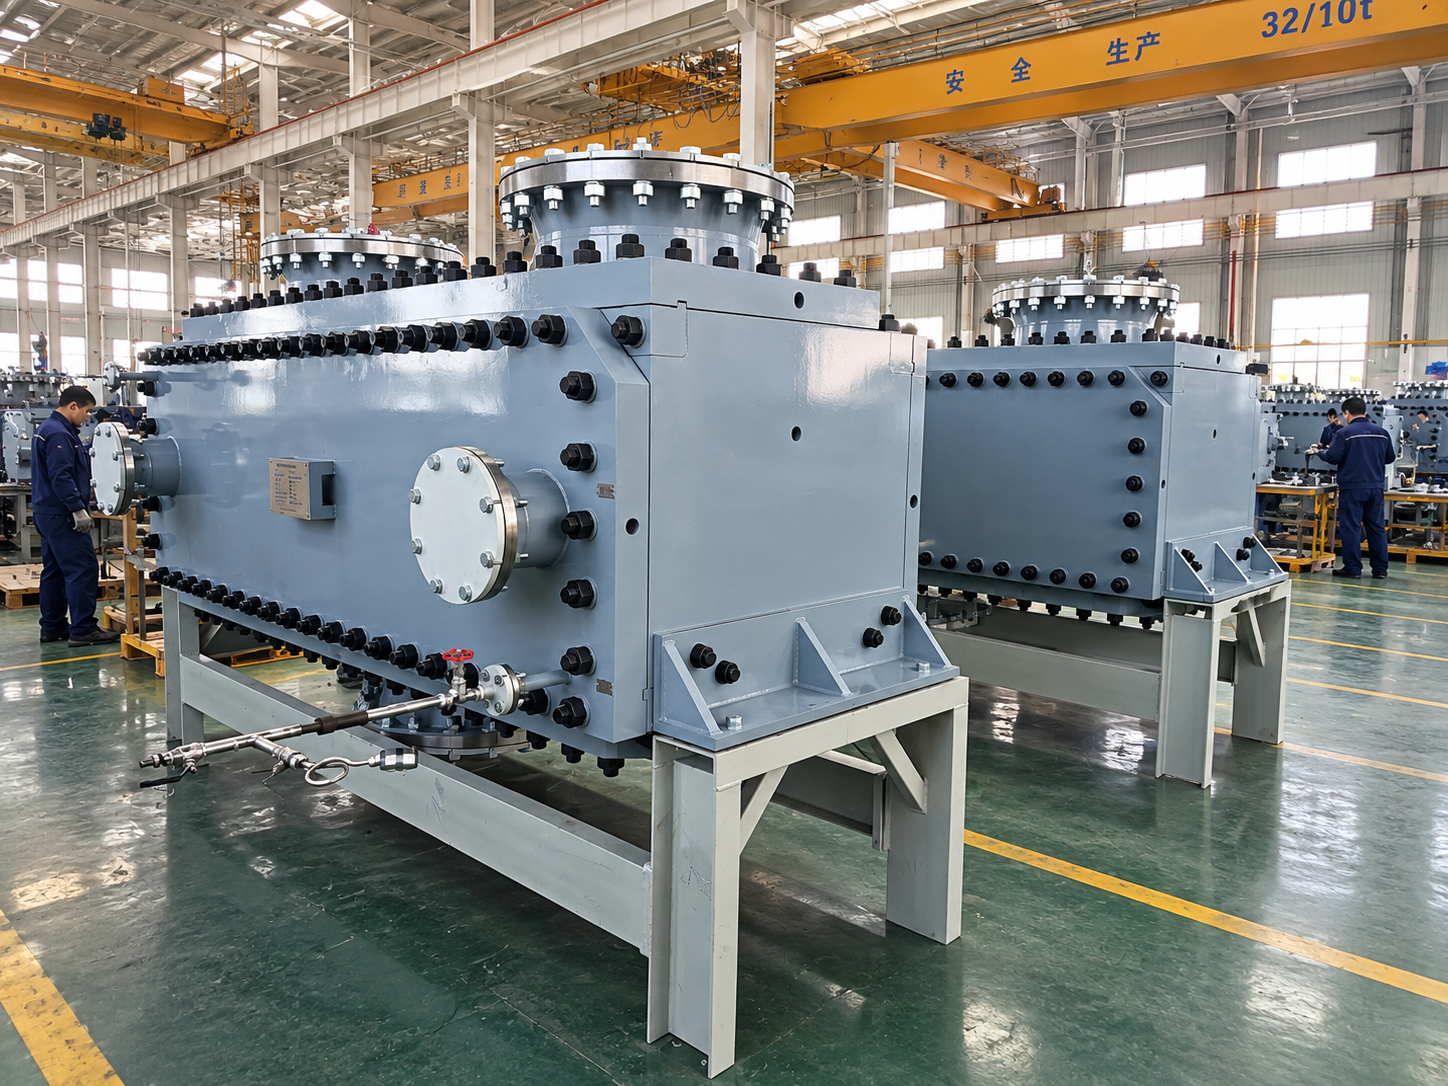
Completed units are connected to test equipment so pressure integrity can be checked before shipment.
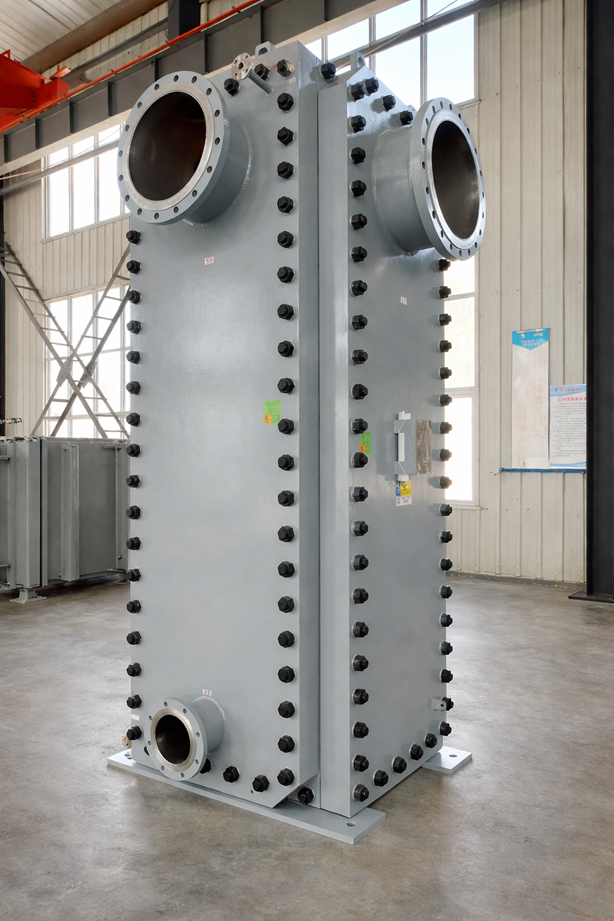
A completed welded plate-and-block heat exchanger configured as a replacement for an installed GEA unit. Final dimensions and connections are confirmed project by project.
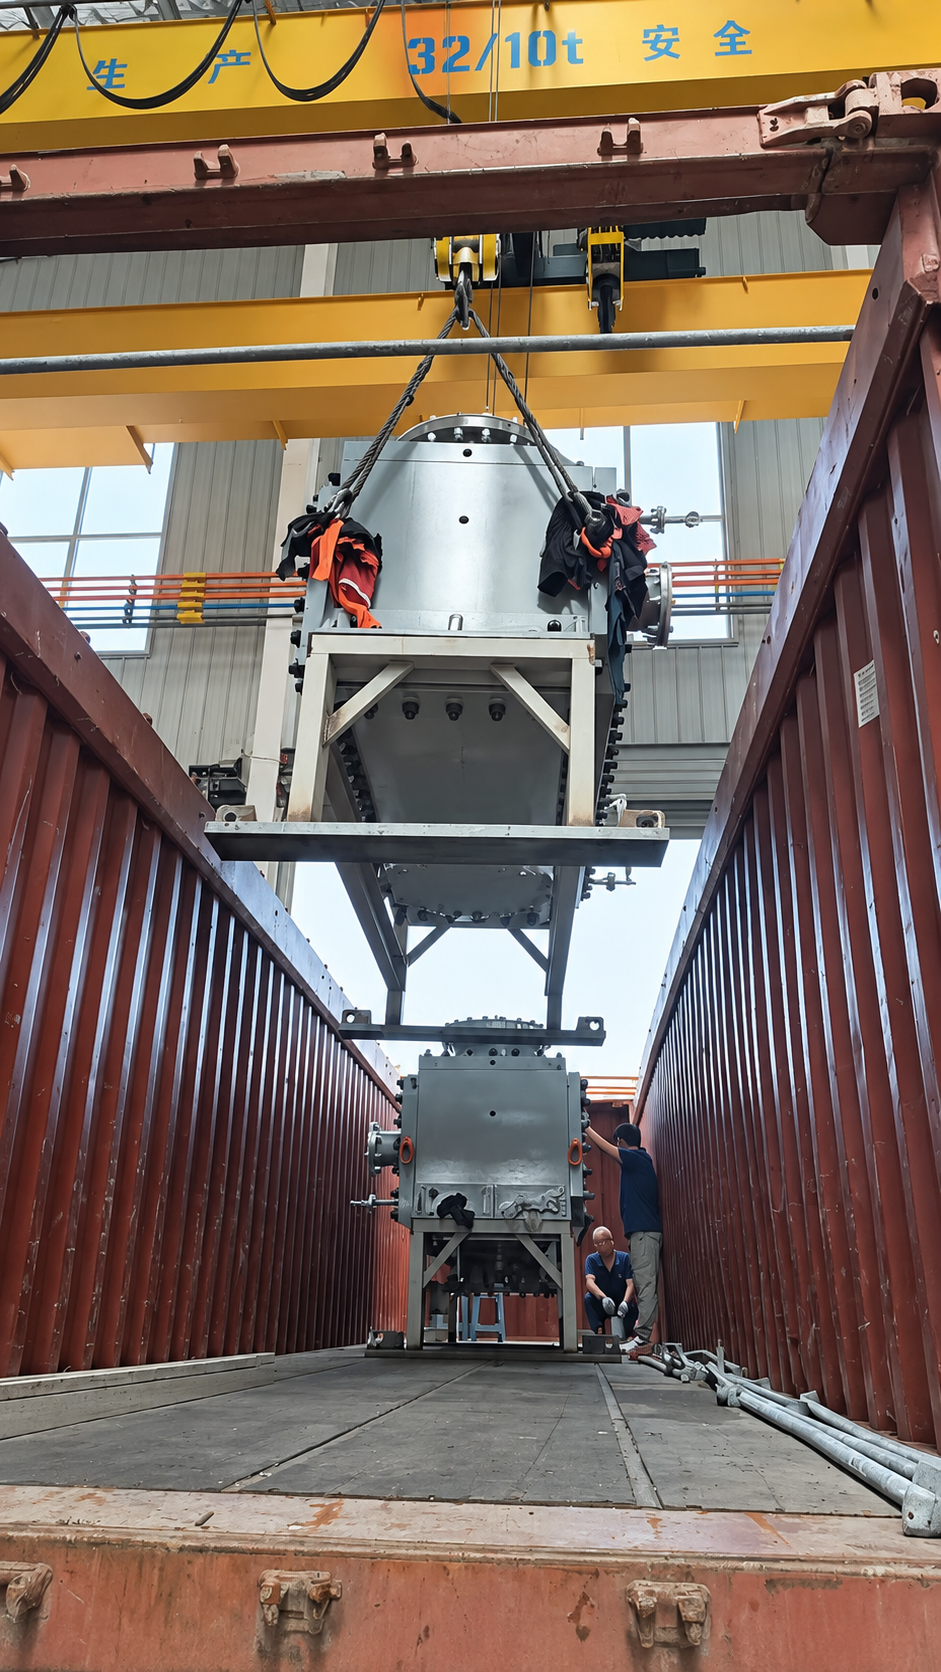
Large units are lifted into the shipping container using the workshop crane and a controlled rigging plan.
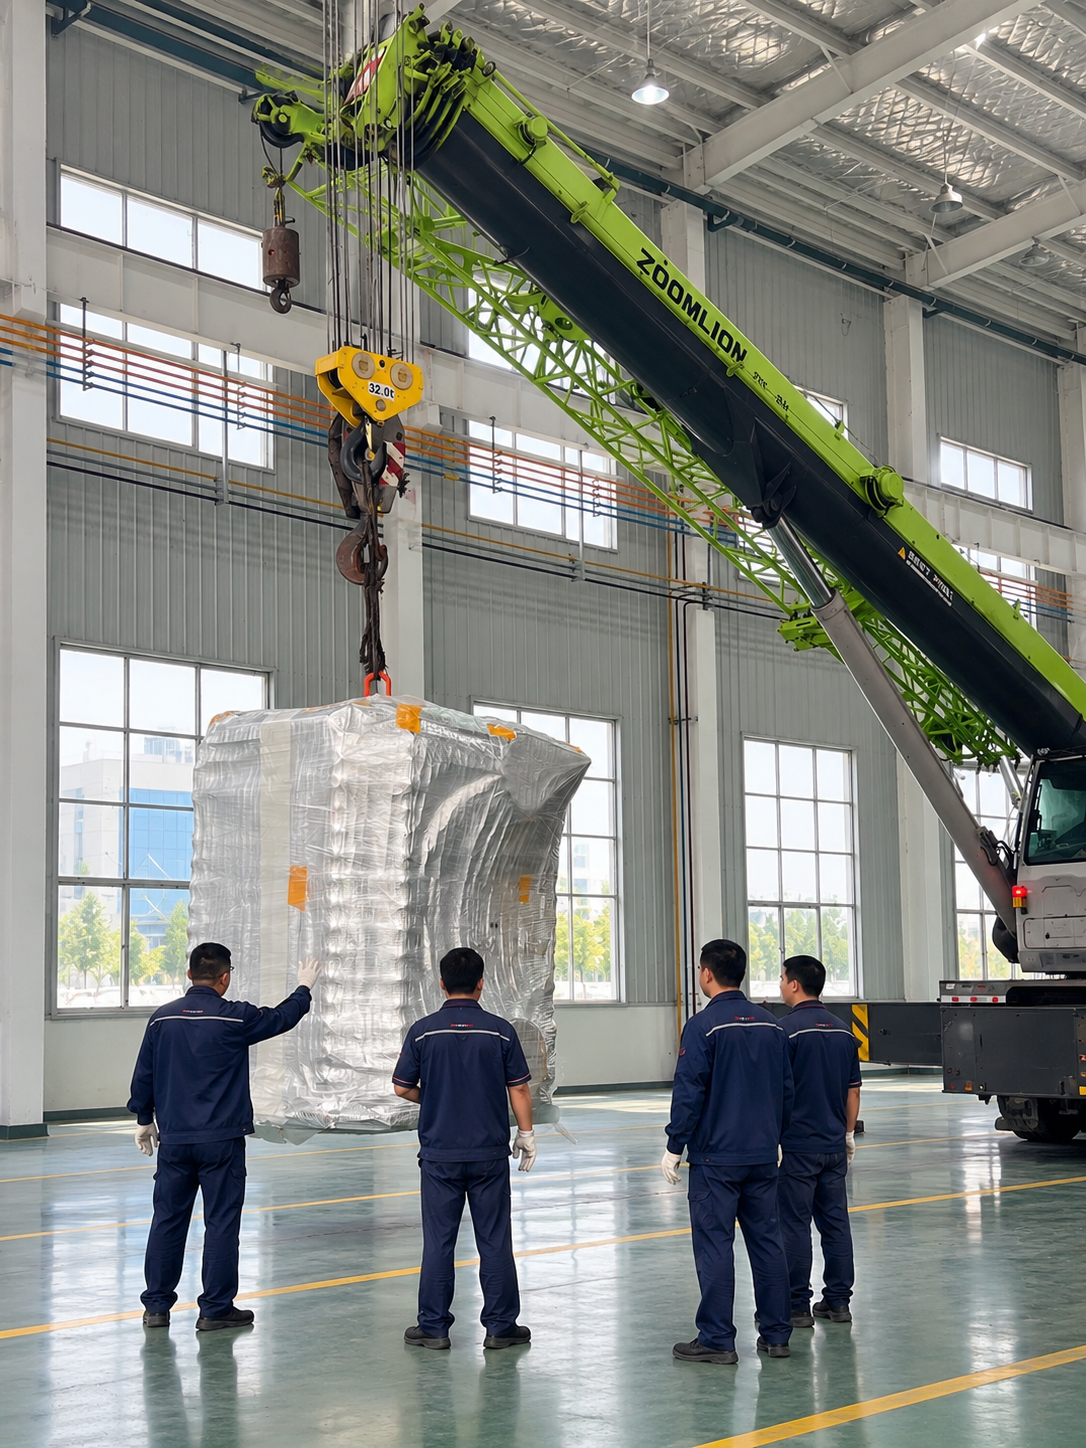
A packaged large-format unit is lifted under controlled supervision before transport.
Selected finished HEXCBLOC units in compact, vertical, horizontal and replacement configurations. Final construction is selected for each project.
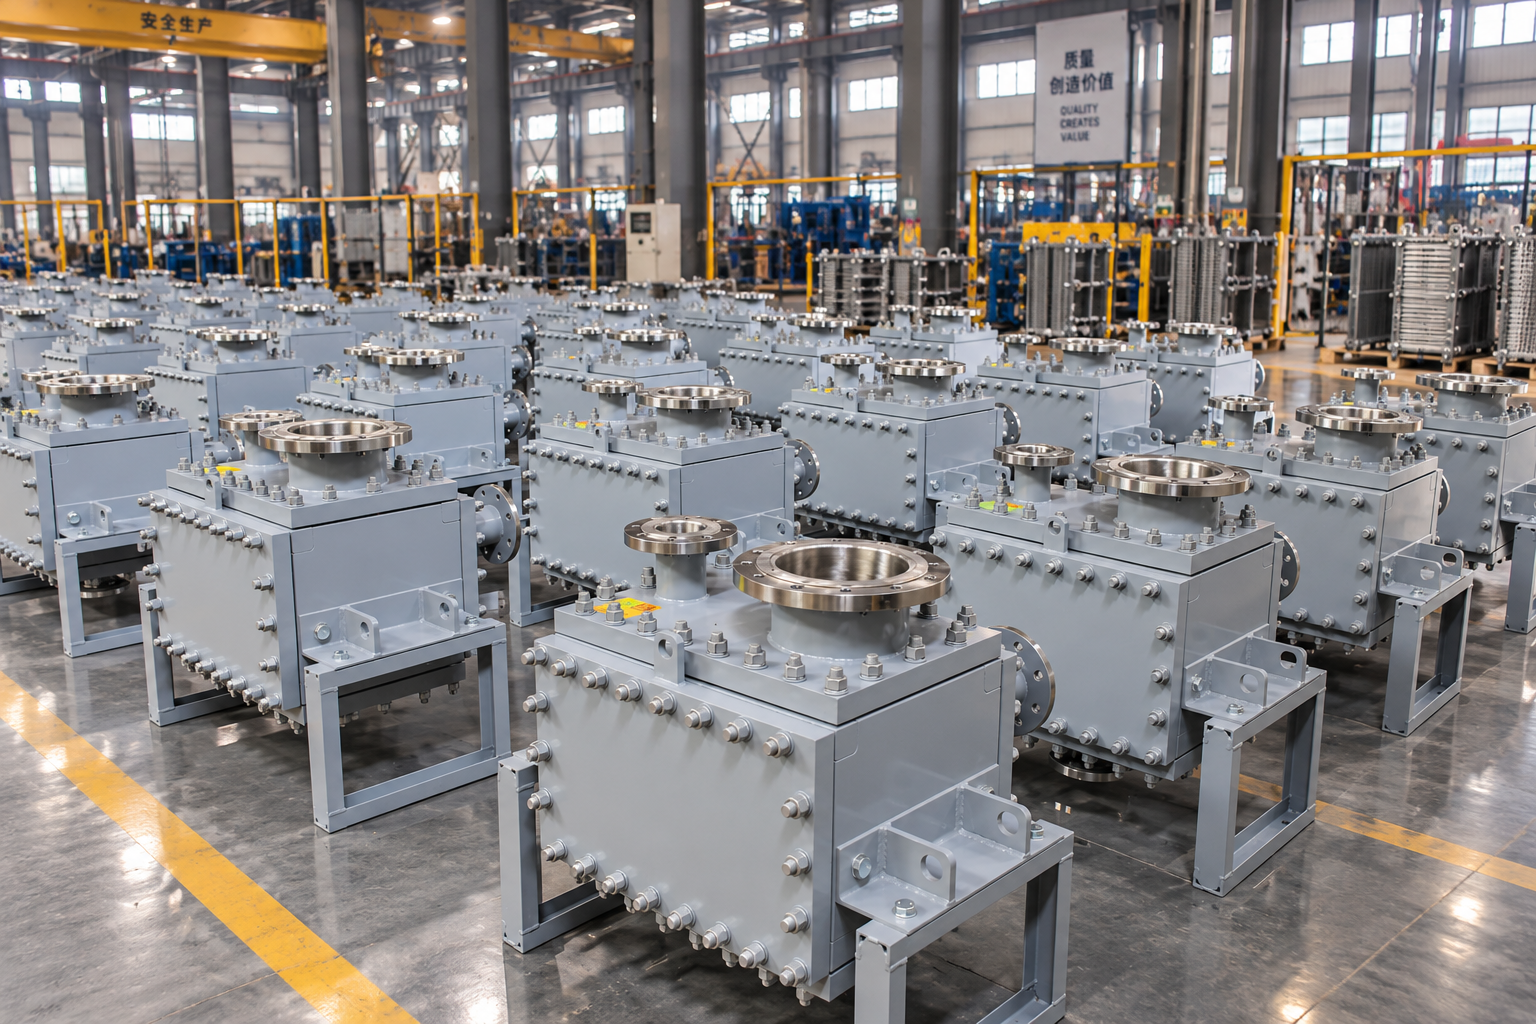
A production batch of finished units in multiple connection and support configurations.
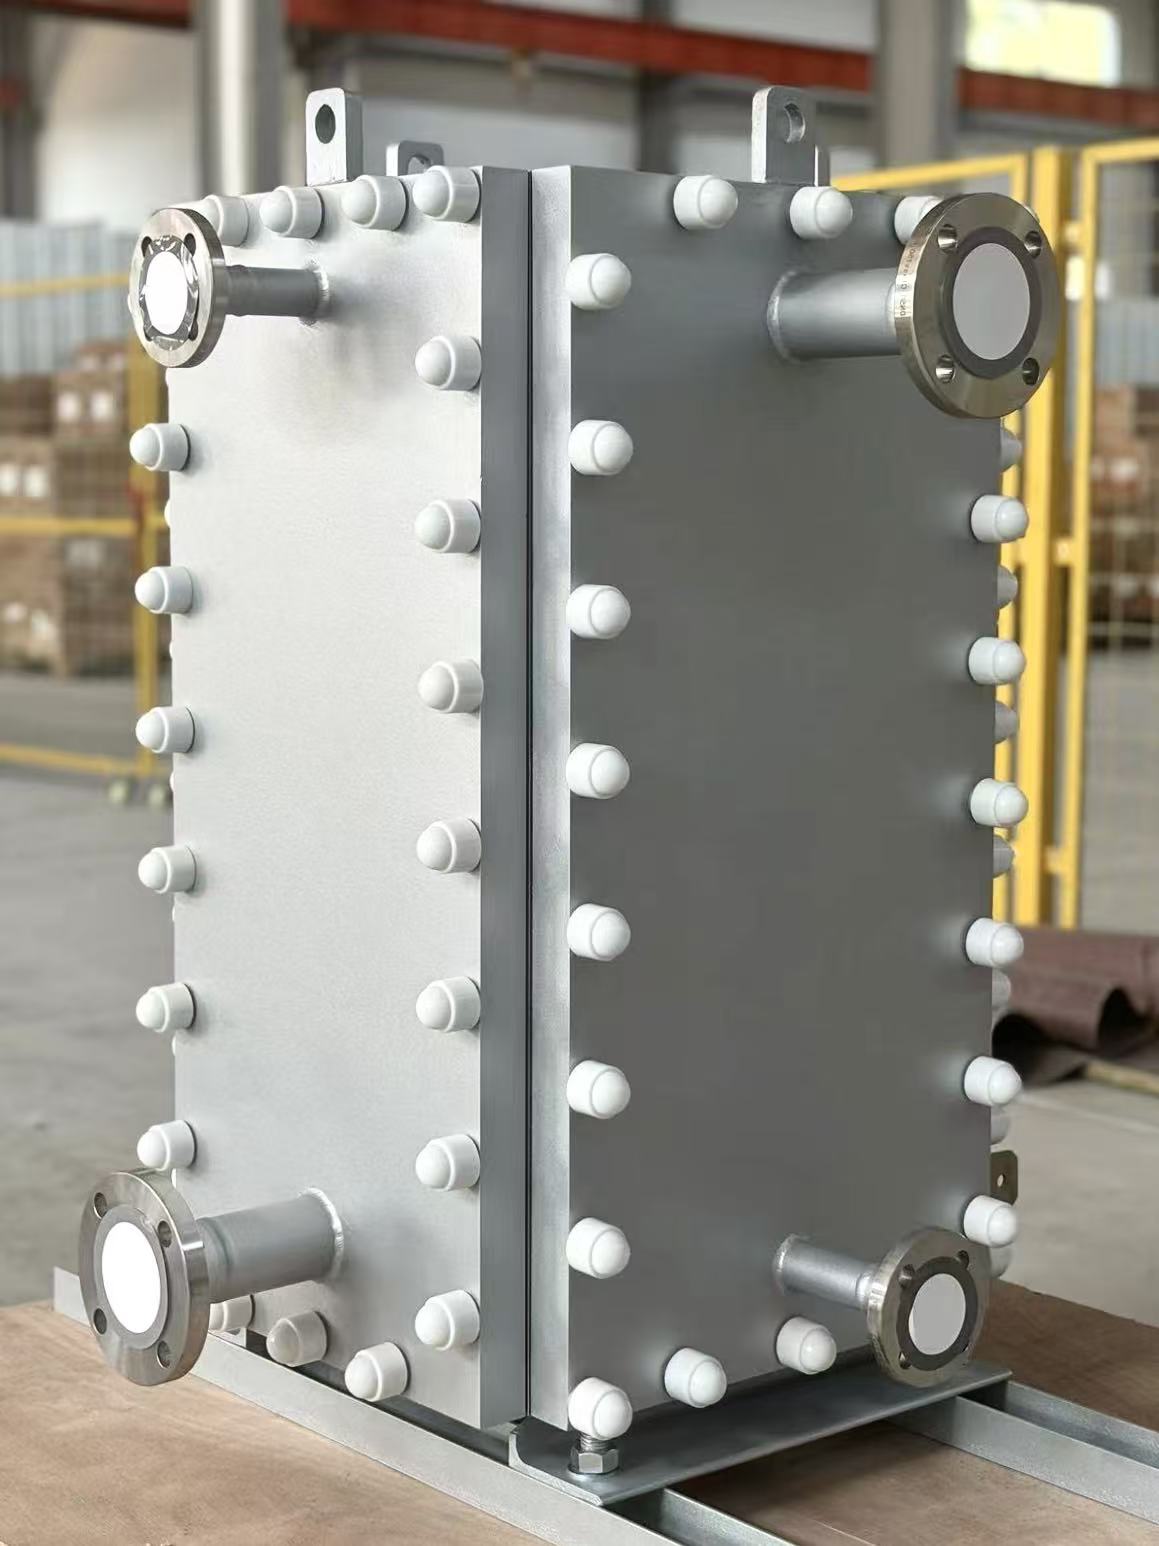
A compact four-connection unit prepared for a replacement duty.
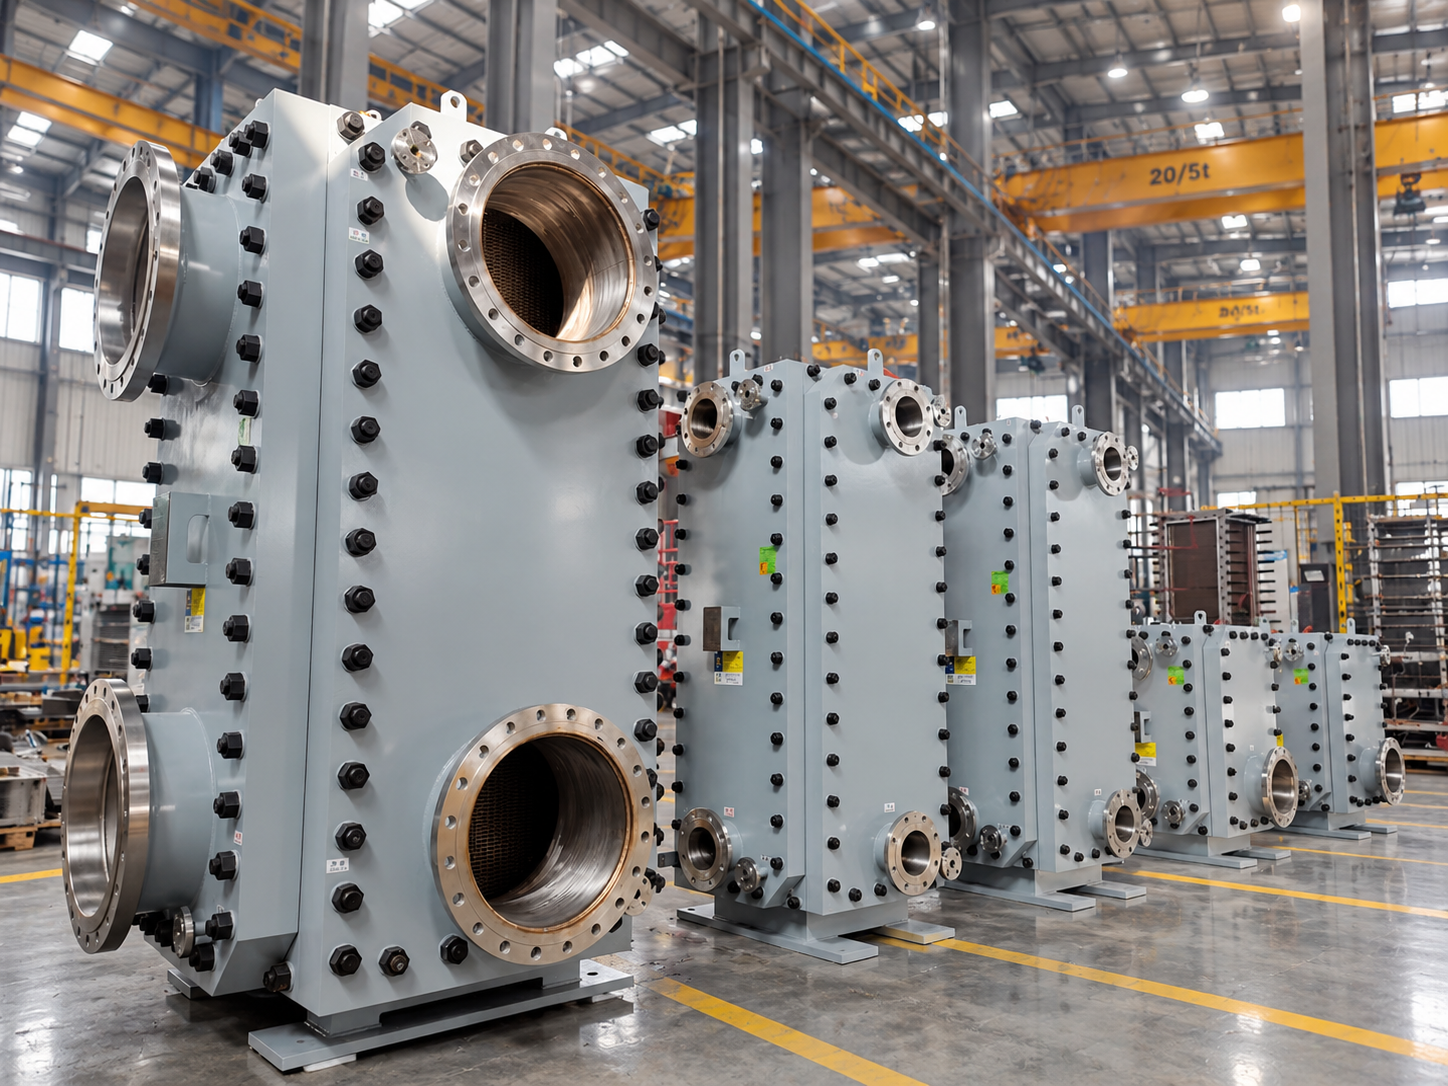
Finished vertical units demonstrate the available range of sizes and connection diameters.
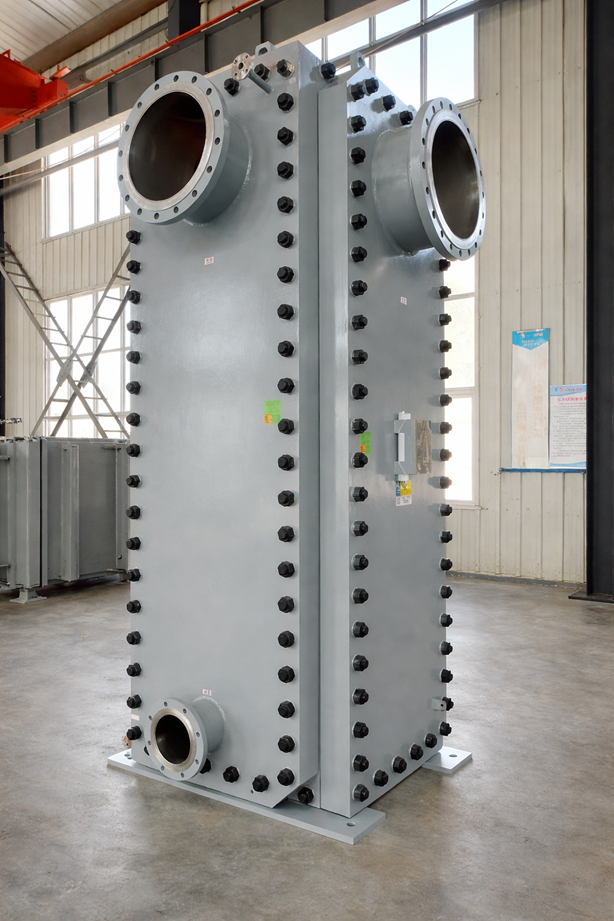
A tall replacement unit configured around the existing installation envelope and nozzle arrangement.
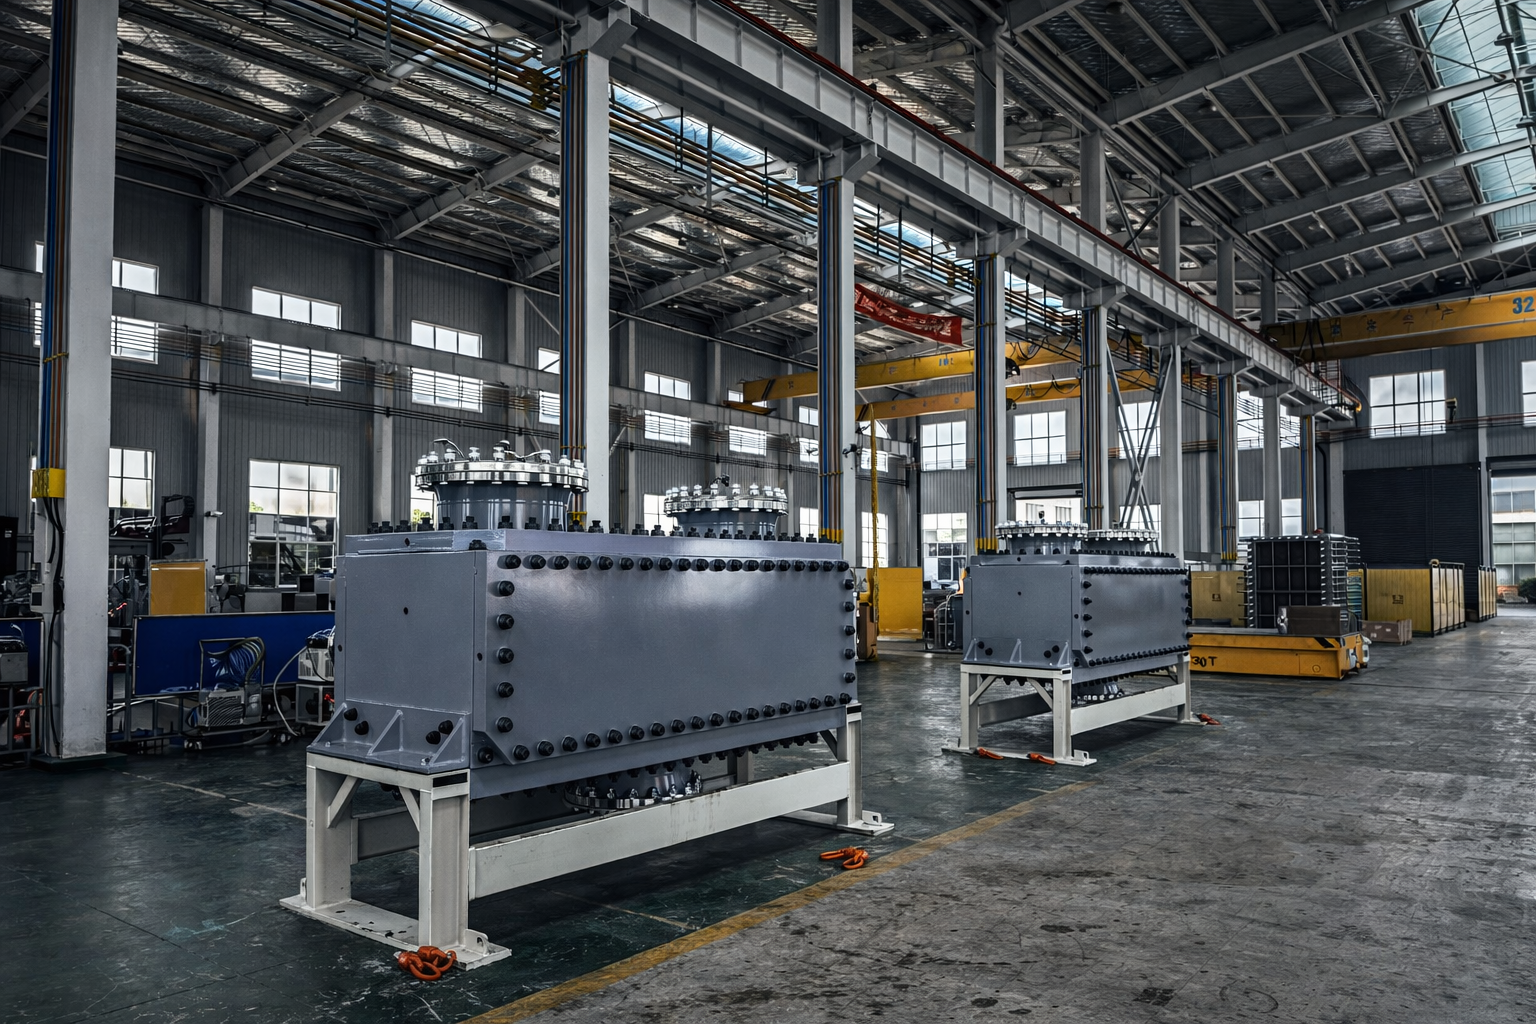
Horizontal units on structural supports for project-specific installation requirements.
View manufacturer certificates, registration documents and their stated scopes.
View CertificationsAgree plate and wetted-part materials, the design code and required material records.
Define inspection stages, pressure-test requirements and any customer or third-party witness points in the project scope.
Confirm the datasheet, approved drawing, applicable inspection records and operating instructions before release.
Manufacturer information: Production · Qualifications
Automatic laser welding is part of the documented PANSTAR welded-product manufacturing process. Plate geometry, alloy, joint preparation and the project inspection scope define the fabrication requirements.
Explore plate welding and channel constructionProvide both fluids, flow rates, inlet and outlet temperatures, operating and design pressures, allowable pressure drop and material requirements. For a replacement, include the nameplate and arrangement drawing.
Explore Compabloc core or complete-unit replacement and K°Bloc complete-unit replacement. Share the datasheet, drawing and operating conditions for review.
Explore Replacement Solutions ↗